HVAC components for manufacturing leak testing

Industry Solutions

HVAC & Refrigeration Leak Testing

HVAC and refrigeration manufacturers use production leak testing to evaluate sealed components and refrigerant circuits before assembly.

Coils, heat exchangers, compressors, valves, fittings, refrigerant lines and manifolds each need a repeatable connection, fixture and test sequence built around the component and manufacturing process.

Air leak testing and trace-gas leak testing are peer options. The appropriate path depends on the component, its internal volume, the manufacturer’s allowable leak target and the production station.

For production helium testing, Z-Charge supplies part preparation and air-test control; Z-Ion supplies helium mass-spectrometer detection. The part, fixture and recipe must be qualified together against the manufacturer’s acceptance requirement.

Request for Quote

What gets tested

HVAC and refrigeration products often combine sealed volumes with intentional flow paths. A useful production test distinguishes those needs and accounts for the part, fixture, added volume and stabilization time.

Zaxis configures production test instruments and fixtures; the manufacturer defines the component acceptance criteria and validates the method for its quality process.

•Evaporator and condenser coils•Heat exchangers•Compressors•Valves and fittings•Refrigerant lines•Manifolds

Methods used

Choosing the method

Select a method around sealing access, component volume, allowable leak target and the production workflow. Air and trace-gas methods are peer lines—not substitutes by default.

Pressure decay and vacuum decay

Pressure decay applies air to a sealed component, isolates the source and measures a defined pressure change. Vacuum decay evacuates a sealed component and measures movement back toward atmospheric pressure.

These air methods can support repeatable production decisions when the fixture, settle time and reject target are defined for the component.

Compare pressure and vacuum decay →

Mass flow for larger volumes or flow paths

Mass-flow testing measures gas moving through a connected component against programmed flow values. It can suit components with an intentional path and can be considered when a flow-based approach fits a larger internal volume.

Large volumes require a deliberate test sequence and stabilization plan; the component, fixture and target set the final method.

Read about mass-flow testing →

Trace gas for tighter leak targets

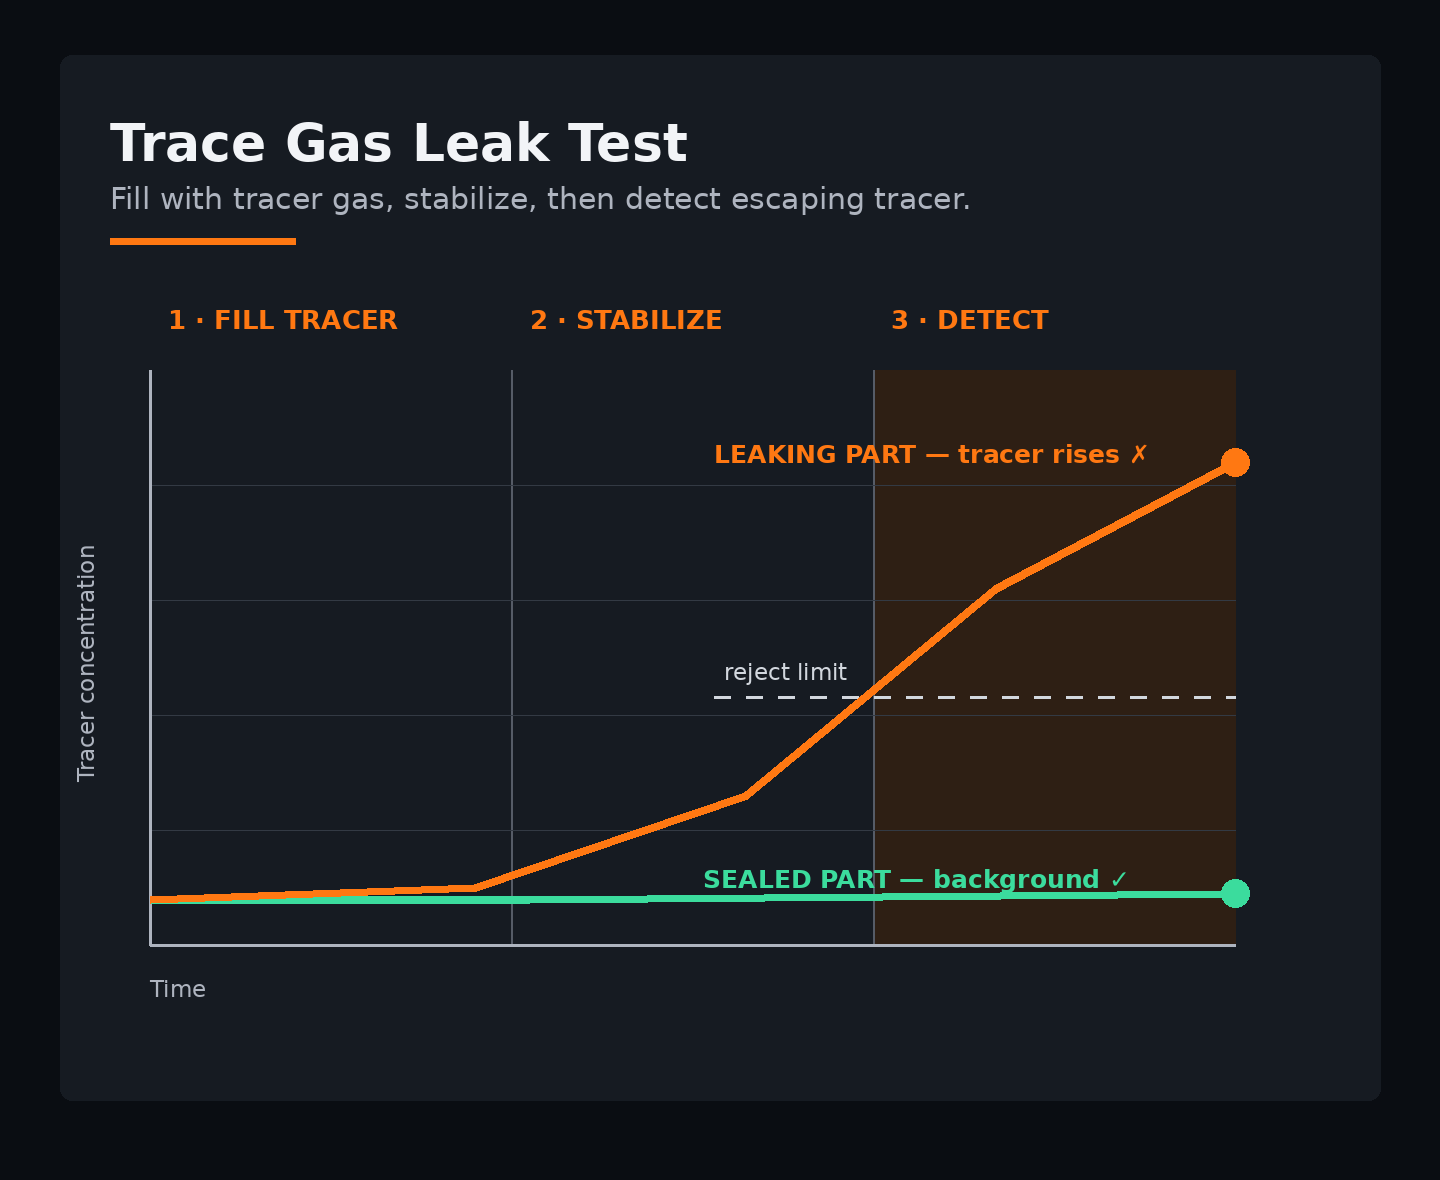
Trace-gas testing fills a sealed part with a measurable tracer and detects gas escaping from the part. Helium, hydrogen forming gas and argon selection follows the allowable leak target, production environment and detection method.

Z-Charge prepares the part and can coordinate gross-leak, pressure-decay and vacuum-decay checks before Z-Ion performs helium detection.

Hydrogen forming gas and argon require detectors compatible with the selected gas. Z-Ion is a helium detector; do not substitute another tracer without confirming the complete configuration.

Explore trace-gas testing →

Test methods by component

Planning routes for manufactured components, not mandatory methods or acceptance recipes. Air and helium methods are peer choices; helium testing does not guarantee zero lifetime refrigerant loss. Qualify the target, fixture, background and cycle with representative parts.

ComponentRecommended methodWhyZaxis product
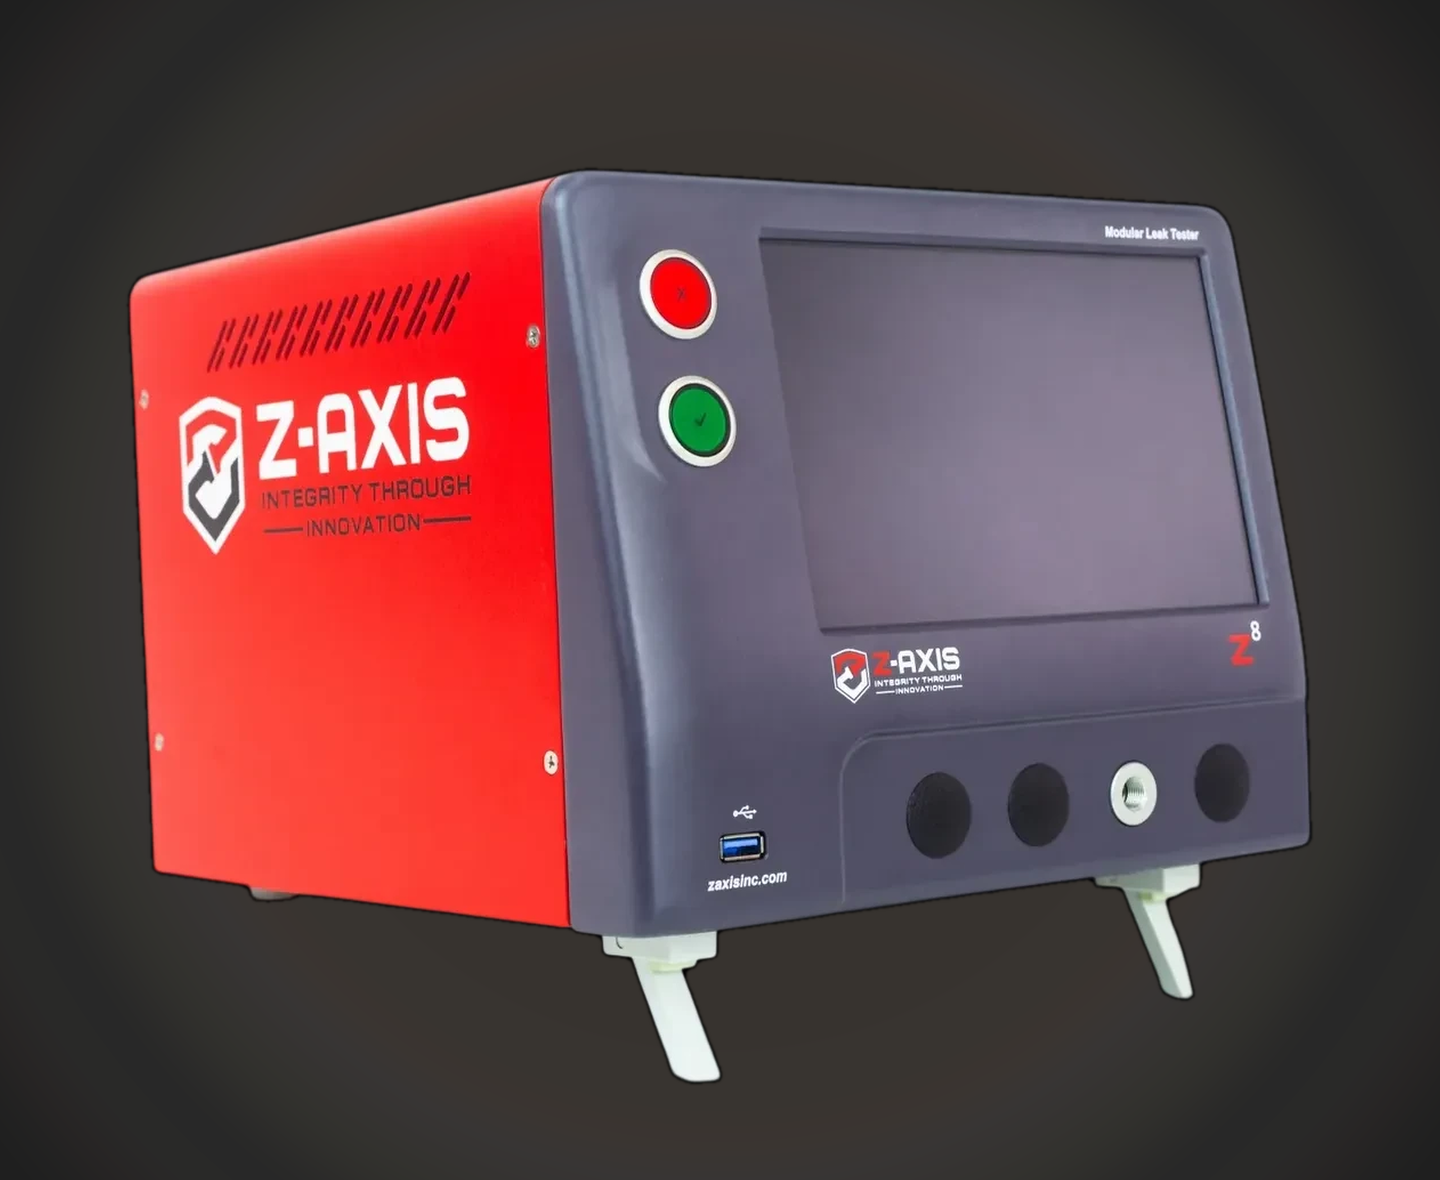
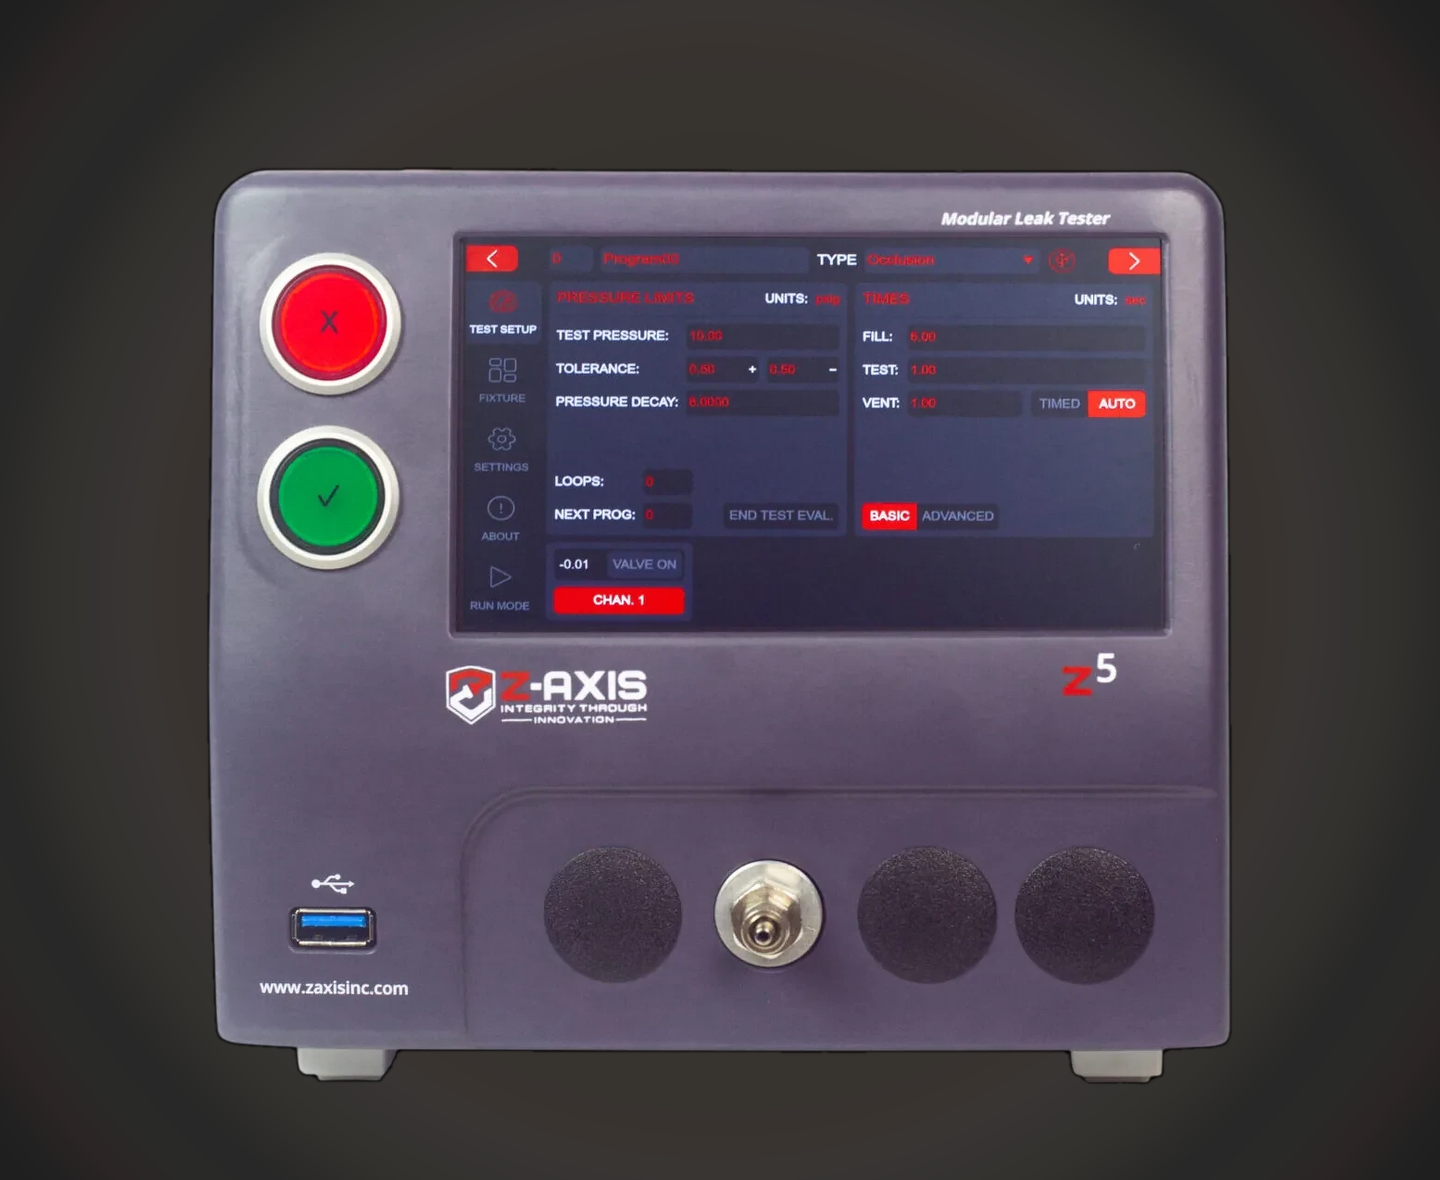
Coils and heat exchangersPressure or vacuum decay; helium sniffing or hard vacuum when requiredSeal ports, account for internal and fixture volume, and retain access to brazed joints.Z5 or Z8 for air; Z-Charge + Z-Ion for helium
CompressorsPressure or vacuum decay; selected helium methodDefine the sealed boundary and distinguish intended flow paths from leaks.Z-Charge preparation/air control + Z-Ion helium detection
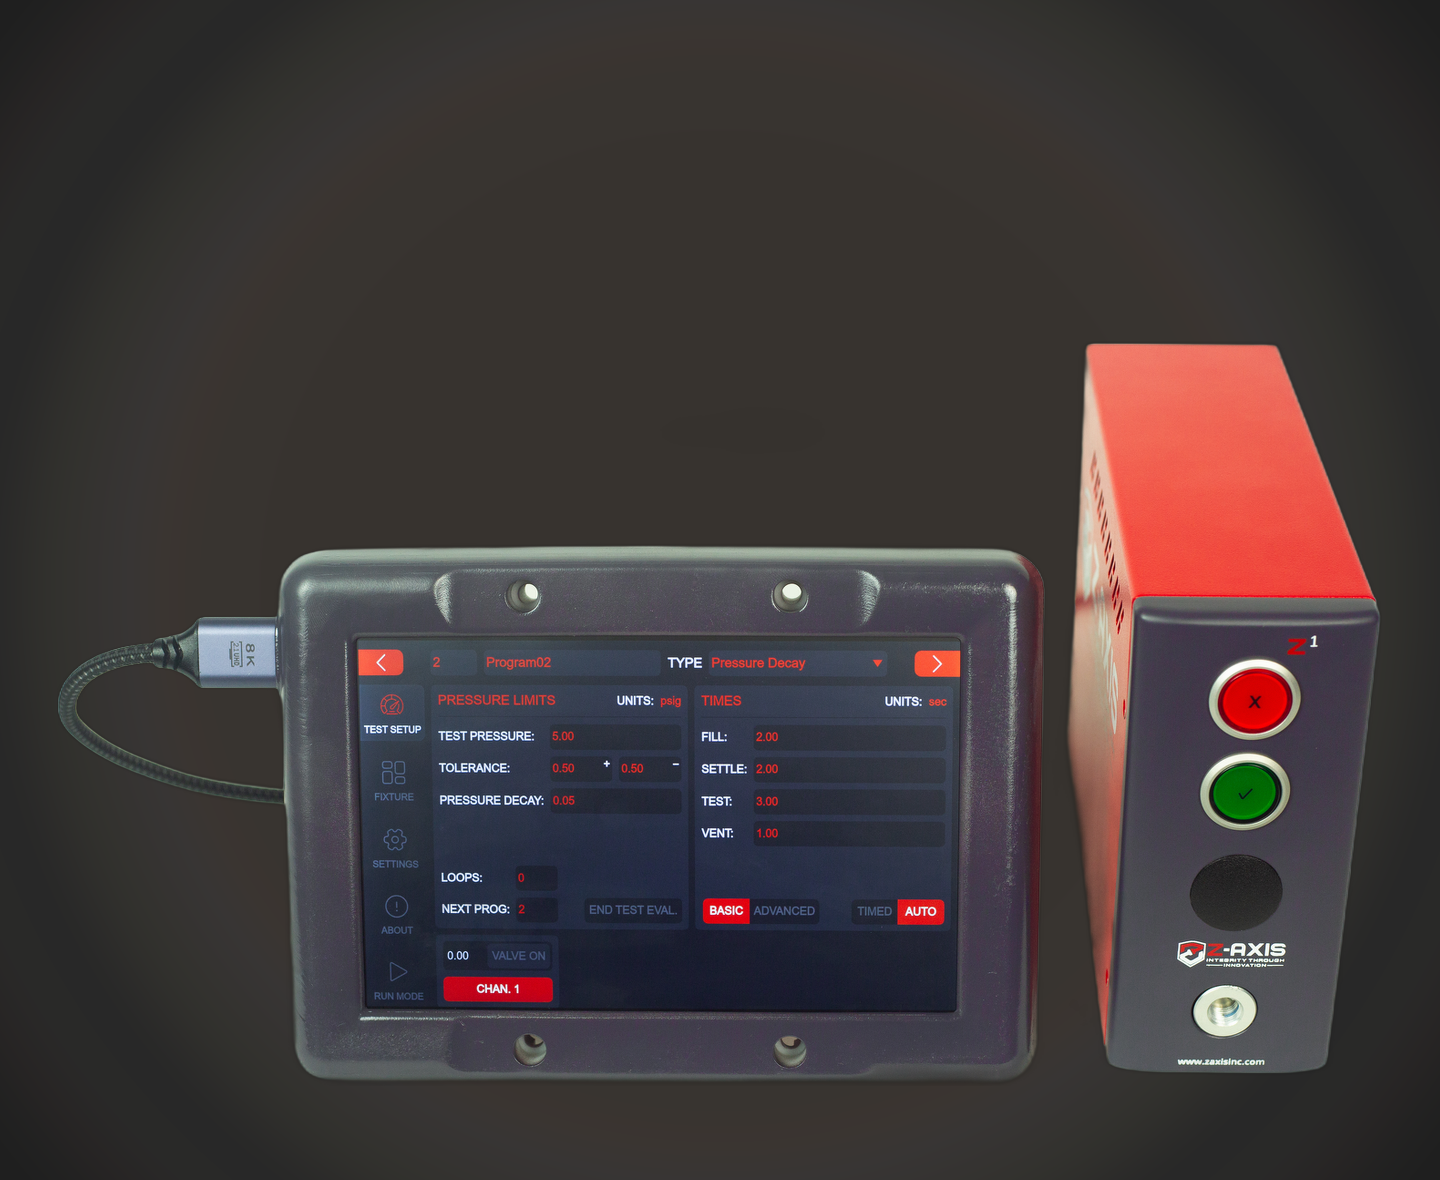
Valves and fittingsPressure decay or mass flow; helium sniffing for localizationDefine valve state, closures and accessible seal faces.Z1 or Z5 for air; Z-Charge + Z-Ion for helium
Refrigerant lines and manifoldsPressure or vacuum decay; helium sniffing or accumulation as selectedClose each branch repeatably and qualify the added connections and volume.Z8 for air; Z-Charge + Z-Ion for helium

Which Zaxis testers fit

Route air applications by port count, fixture, pressure and automation needs. Z-Charge + Z-Ion provides coordinated preparation and helium detection when the helium method fits the validated target. General forming-gas and argon education does not establish Z-Ion detection of those gases.

Production method, fixture and data

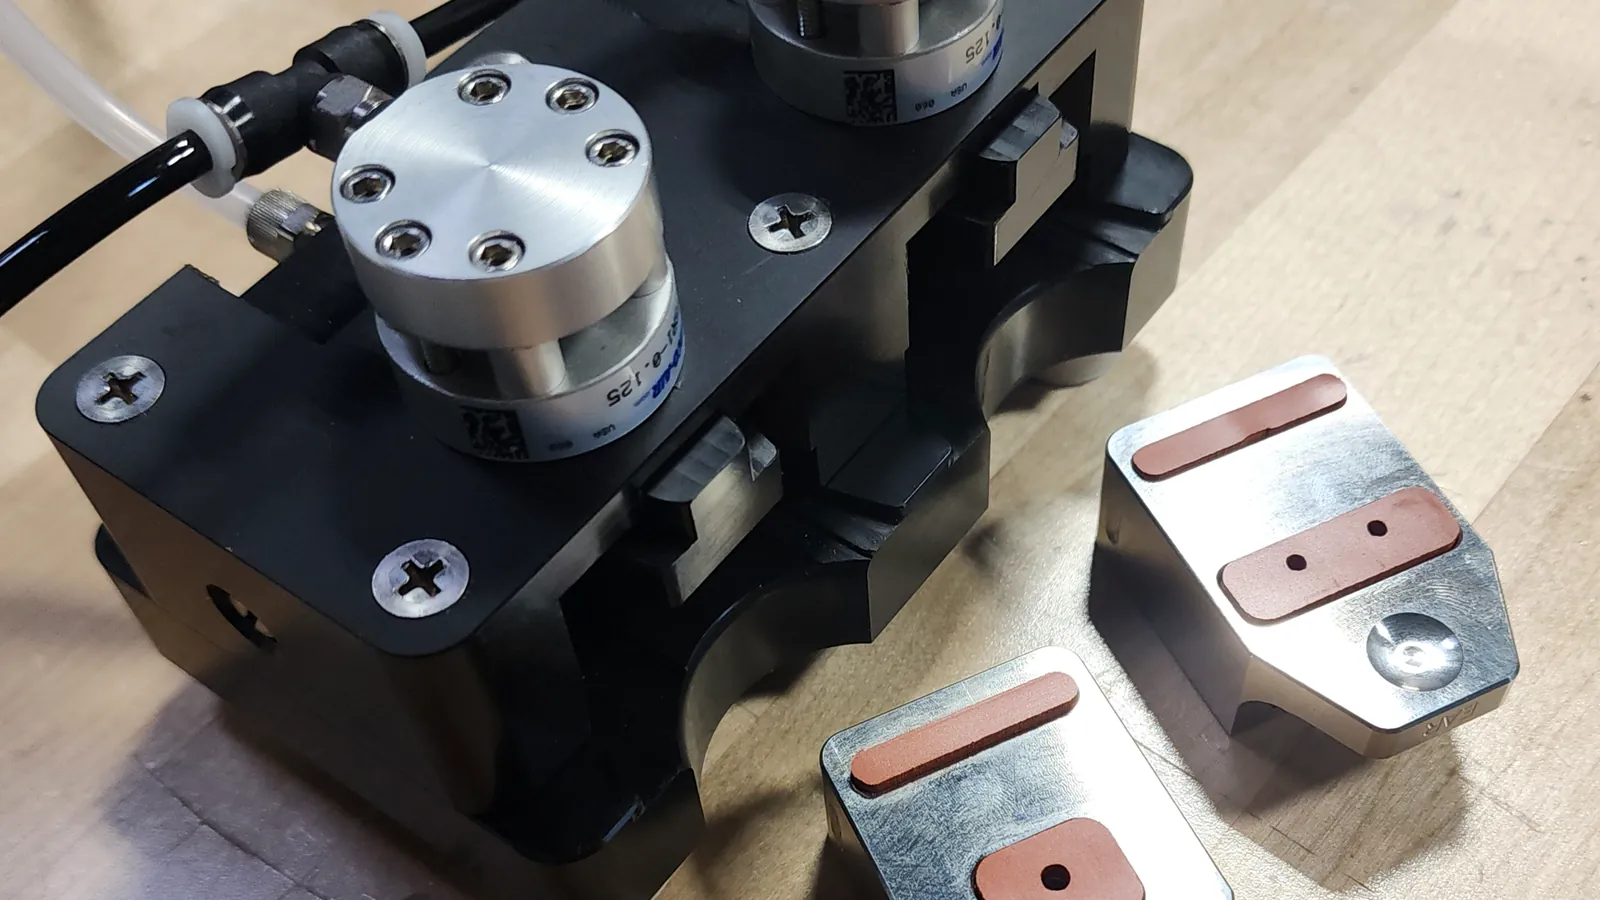
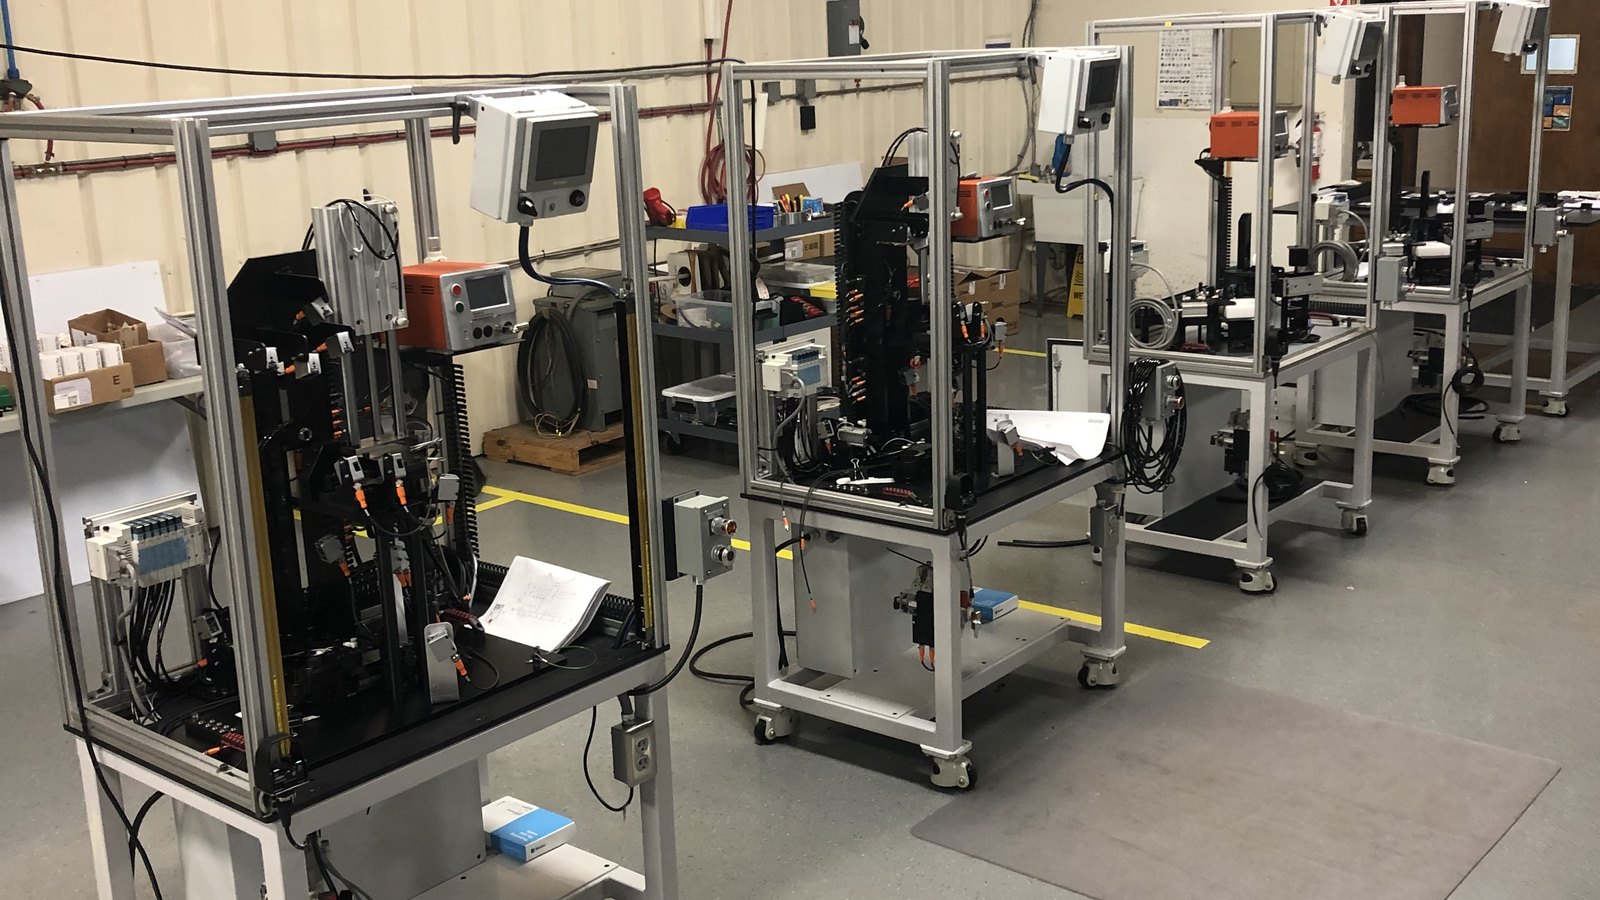
A custom fixture can seal ports, control added volume and create a repeatable connection between a component and the tester. For multi-port parts, the fixture and programmed sequence can isolate or test more than one location.

For automated lines, compatible Zaxis platforms offer connectivity options for PLC integration and production data. Confirm interfaces, traceability requirements and test sequence for the specific platform and line.

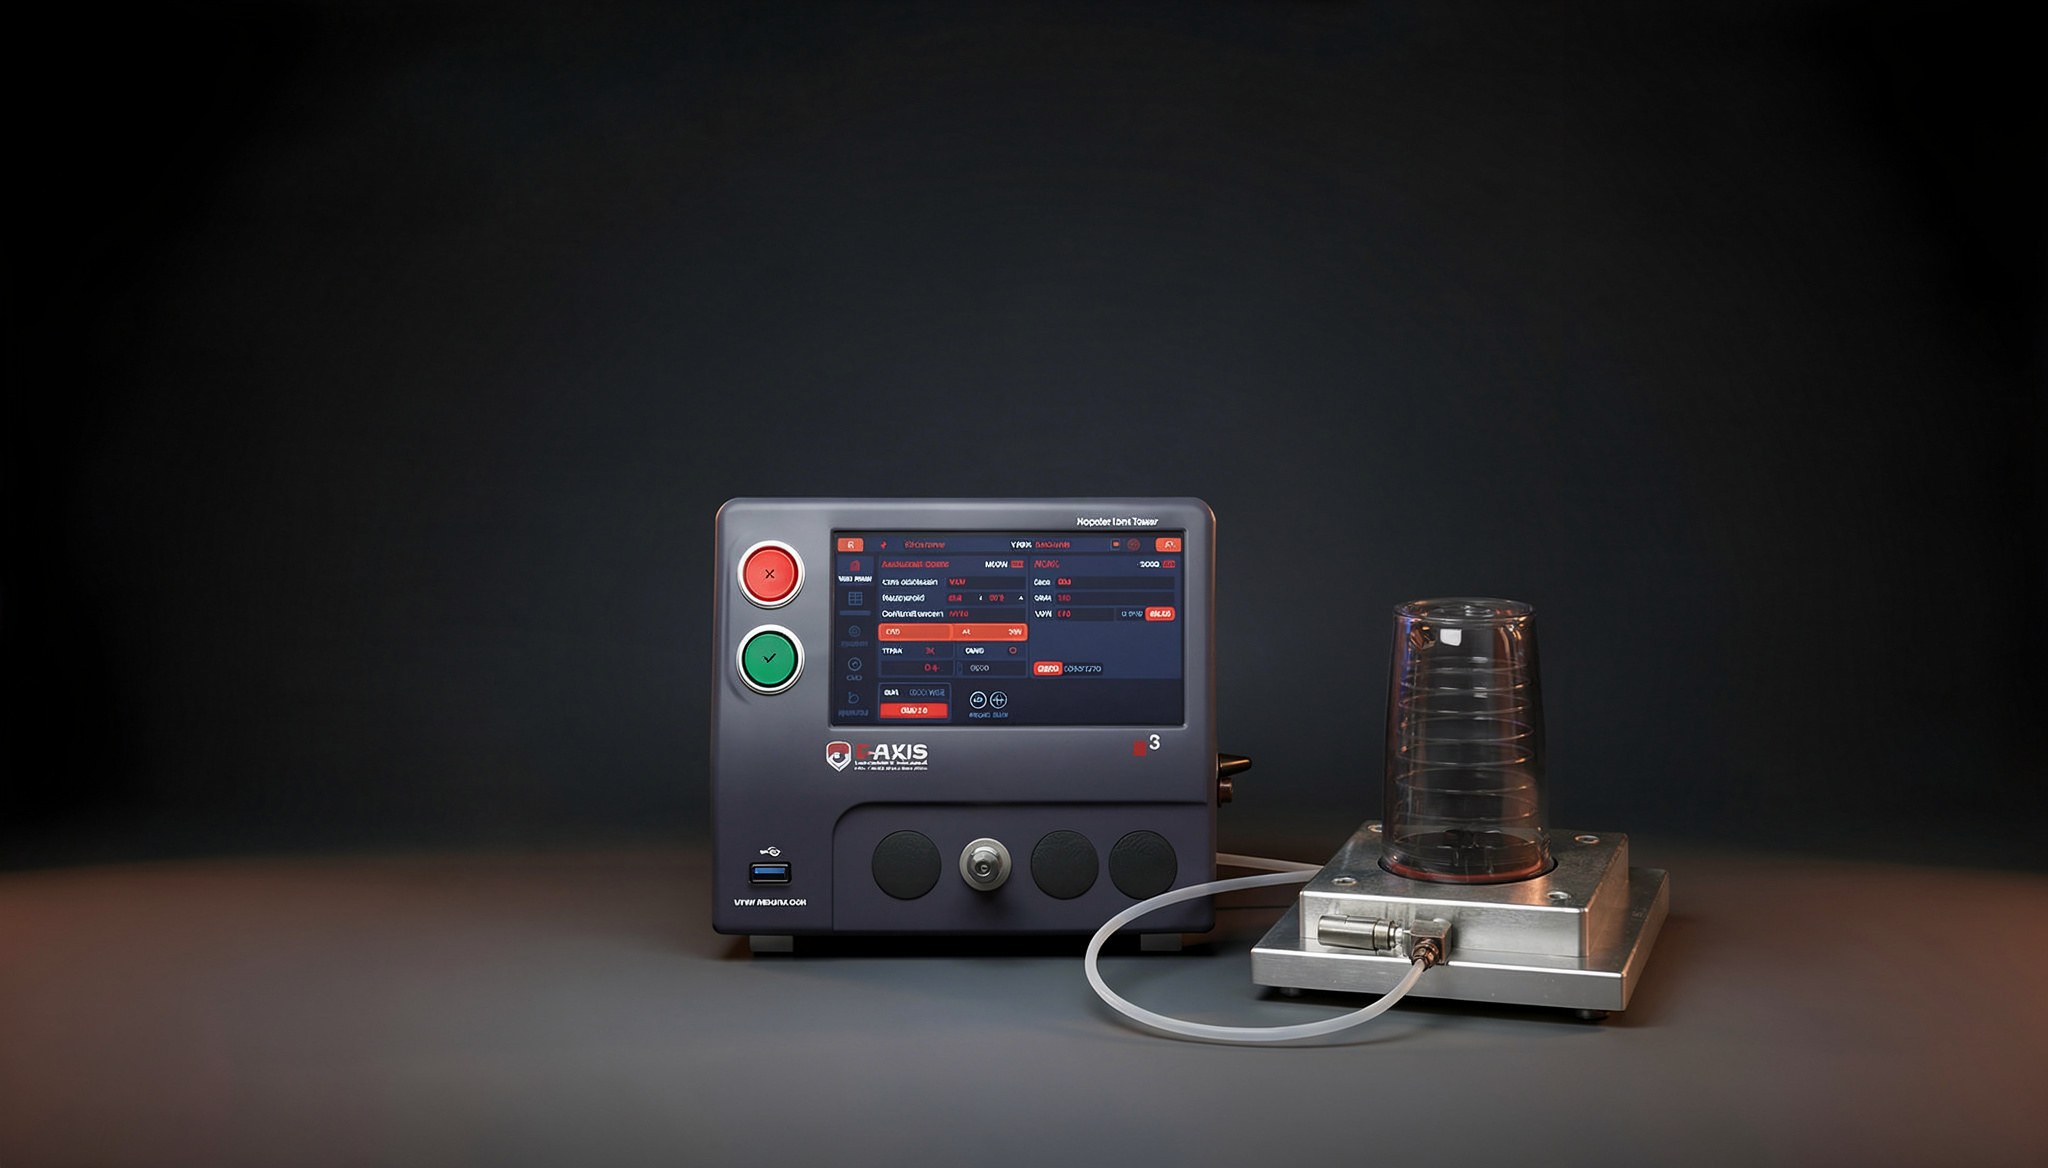
Zaxis leak tester connected to a custom production fixture

In depth: HVAC and refrigeration components

Production helium workflow: prepare, detect and record

Coils and heat exchangers require a fixture and sequence that suit their ports and internal volume. Compressors, valves, fittings, refrigerant lines and manifolds similarly need the test connection and target defined for their product function.

For large-volume components, stability matters. The part, fixture and added test volume should be considered together so the programmed test allows the measurement to settle before a production decision is made.

Seal the component to the fixture and verify the connection before gas flows. A configured recipe can run an optional gross-leak, pressure-decay or vacuum-decay screen, then evacuate, purge and charge helium. Z-Charge commands Z-Ion for the selected sniffing, hard-vacuum, accumulation or bomb sequence.

Associate pass/fail, recipe ID, charge parameters and detector result with the part record. Confirm the PLC interface and data mapping; available communications do not by themselves establish a complete MES implementation. Hard-vacuum work requires an external vacuum source, and chamber/tooling, handling and any recovery equipment belong in the confirmed scope of supply.

For application review, provide the drawing or sample, ports and sealed boundary, internal and fixture volume, allowable pressure/vacuum, leak target and units, refrigerant/test conditions, cycle time, loading plan and required records. Qualify background control, calibration and representative good/defective parts before release. No universal helium requirement, throughput or recovery yield is assumed.
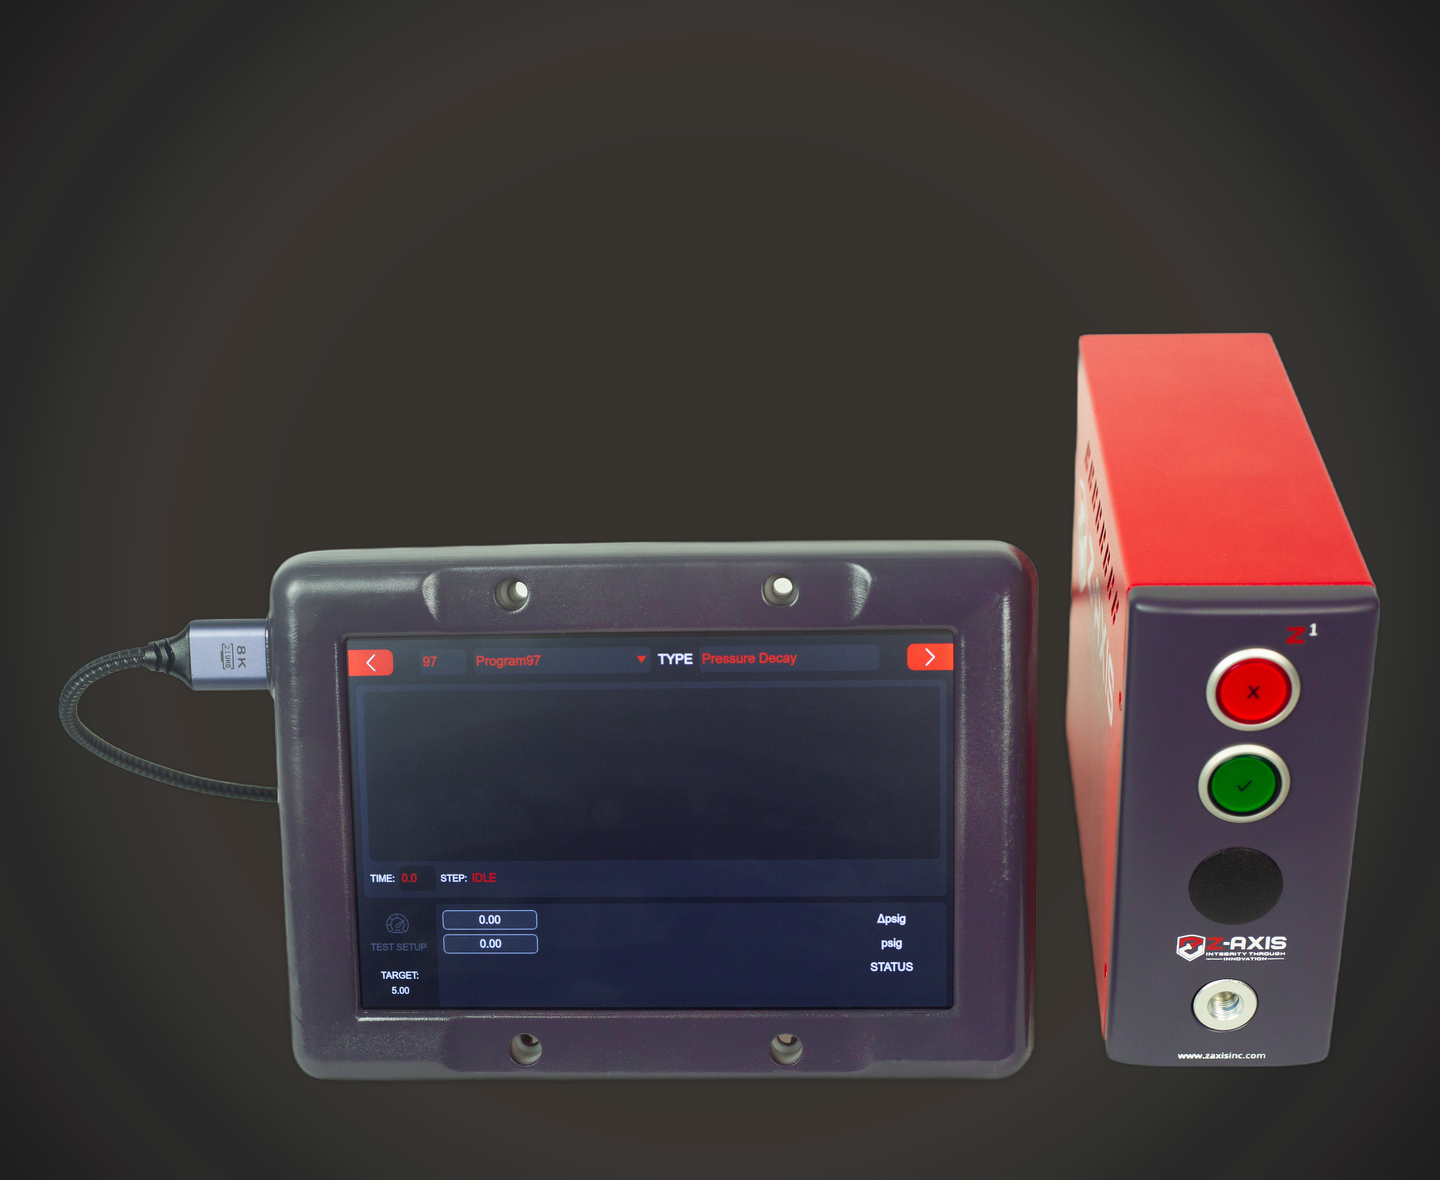
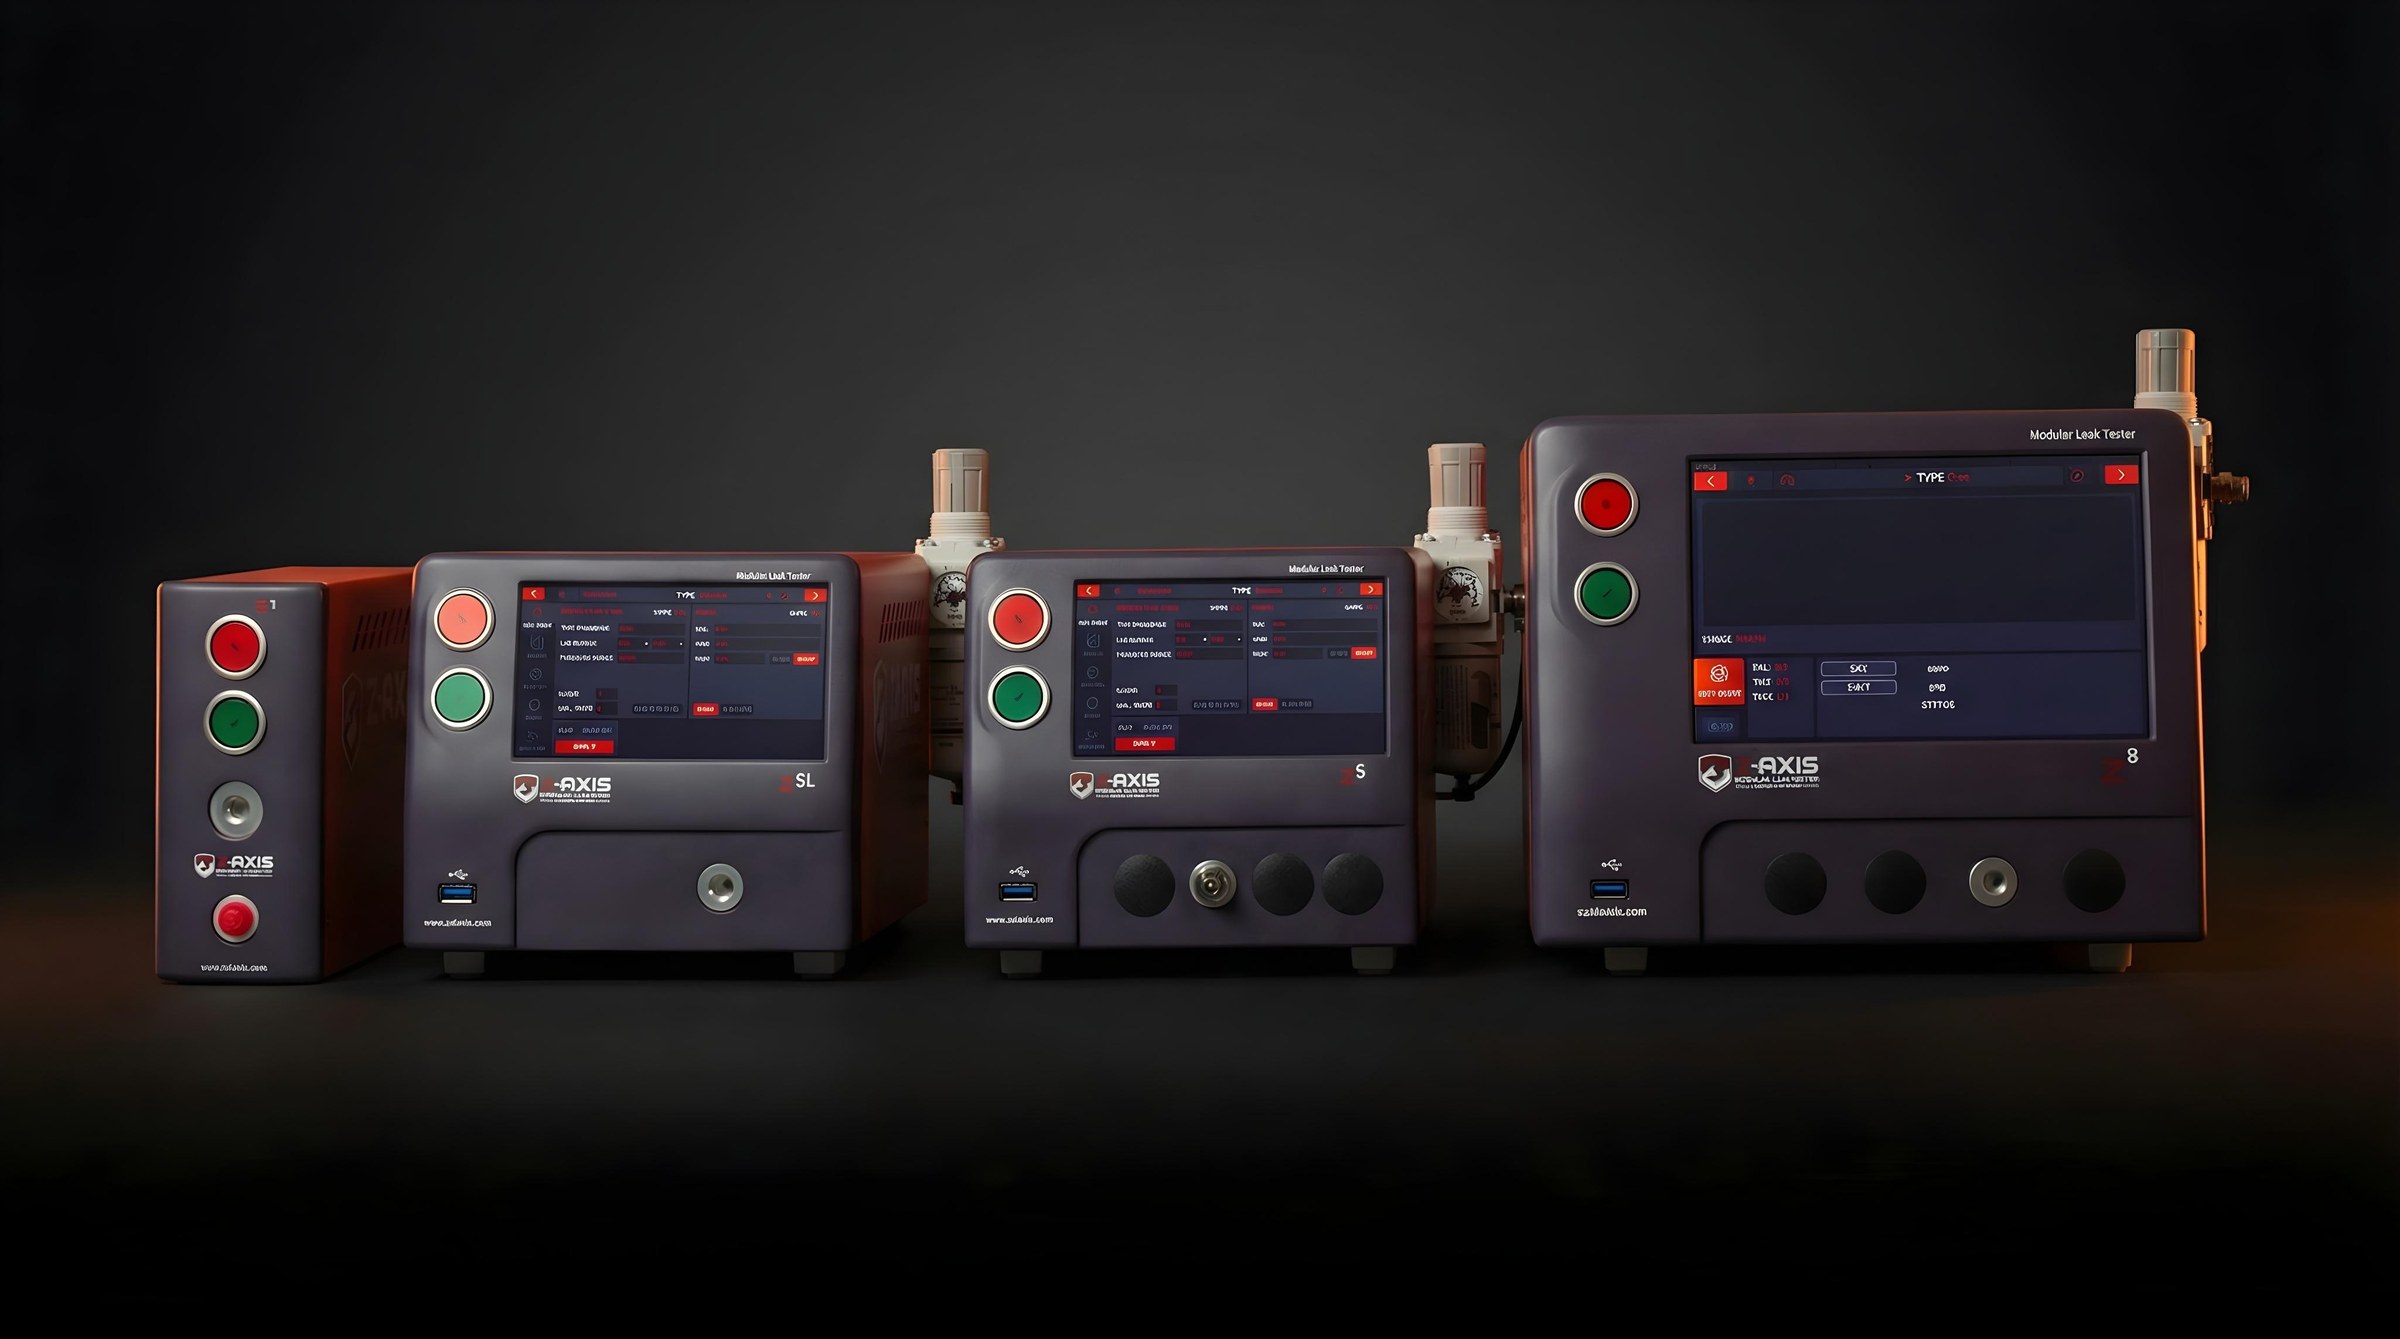
Air leak testers for an HVAC manufacturing test station

Air and trace gas as peer production paths

Air leak testing includes pressure decay, vacuum decay and mass flow. Trace-gas leak testing uses a measurable tracer. A component is not assigned to one family by its industry alone: the final selection follows access, volume, allowable leak target, fixture and production requirements.

Zaxis supports both product lines. Application engineering can help connect the manufacturer’s required target to the appropriate instrument, fixture and sequence.

Trace-gas leak testing measurement graph

Applications in this industry

HVAC coil and heat-exchanger manufacturing context

Coils and heat exchangers

Production test planning can pair coil and heat-exchanger ports, volume and leak target with a configured air or trace-gas method.

Zaxis leak tester connected to a sealed fixture

Compressors, valves and fittings

Sealed compressor, valve and fitting assemblies can use a fixture and test sequence selected around access and the manufacturer’s acceptance criteria.

Zaxis Z1 tester for an automated component station

Refrigerant lines and manifolds

Connected refrigerant lines and manifolds may use a pressure, vacuum, flow or tracer approach selected around the circuit and production requirement.

HVAC & Refrigeration Leak Testing FAQ

What is HVAC and refrigeration leak testing?

It is production testing of HVAC and refrigeration components such as coils, heat exchangers, compressors, valves, fittings, refrigerant lines and manifolds using a method and fixture selected for the component.

Which method fits a heat exchanger or coil?

Pressure decay, vacuum decay, mass flow or trace gas can be considered depending on the component’s access, internal volume, allowable leak target and production requirements. The manufacturer validates the final method and acceptance criteria.

When is mass flow considered for HVAC components?

Mass flow can be considered for an intentional flow path or when a flow-based approach fits a larger-volume component. The test sequence needs suitable stabilization time for the part and fixture.

When is trace-gas testing considered for a refrigerant circuit?

Trace gas can be considered when a measurable tracer and the selected detection method fit the manufacturer’s required leak target. Air and trace-gas testing are peer production methods.

Why does fixturing matter?

A fixture seals the component, controls added test volume and provides repeatable connections. It can also close multiple openings or support a multi-port sequence.

Can a Zaxis test station connect to automation?

Compatible platforms offer connectivity options for PLC integration and production data. Confirm the interface and traceability approach for the selected platform and line.

Plan your HVAC or refrigeration leak-test station

Request for Quote
Zaxis leak tester product lineup