FILL
Connect the part with a fitting or fixture and pressurize it to the desired test pressure.
Leak Test Method
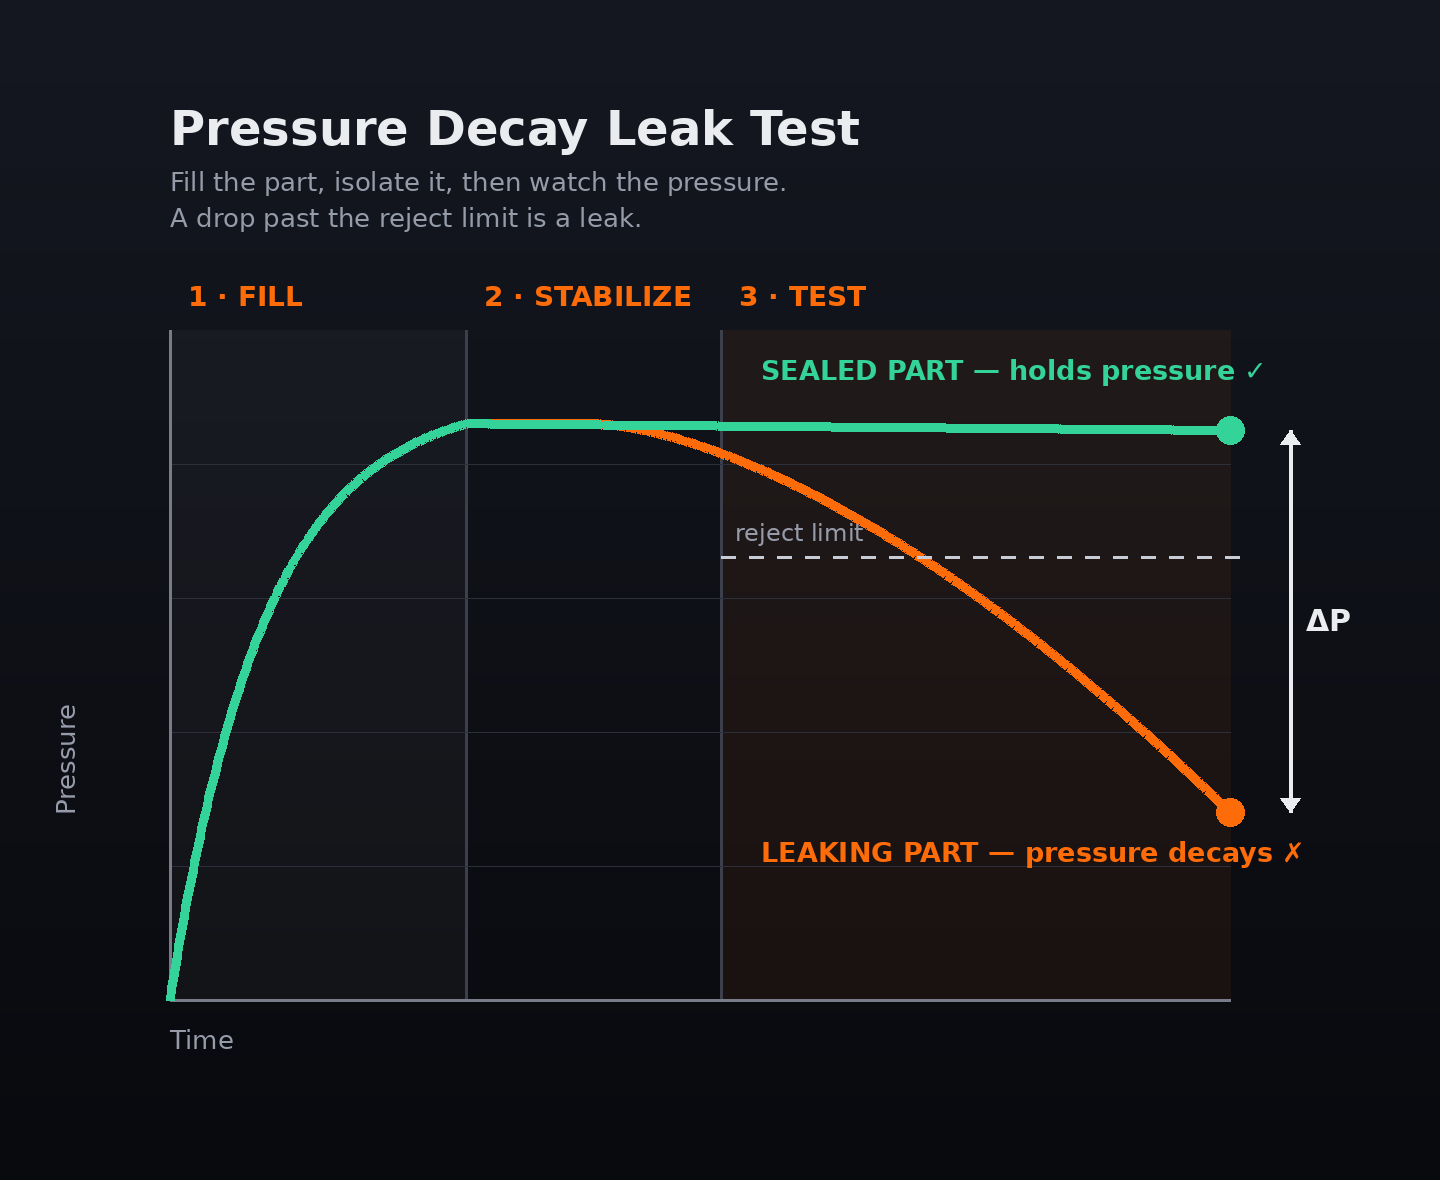
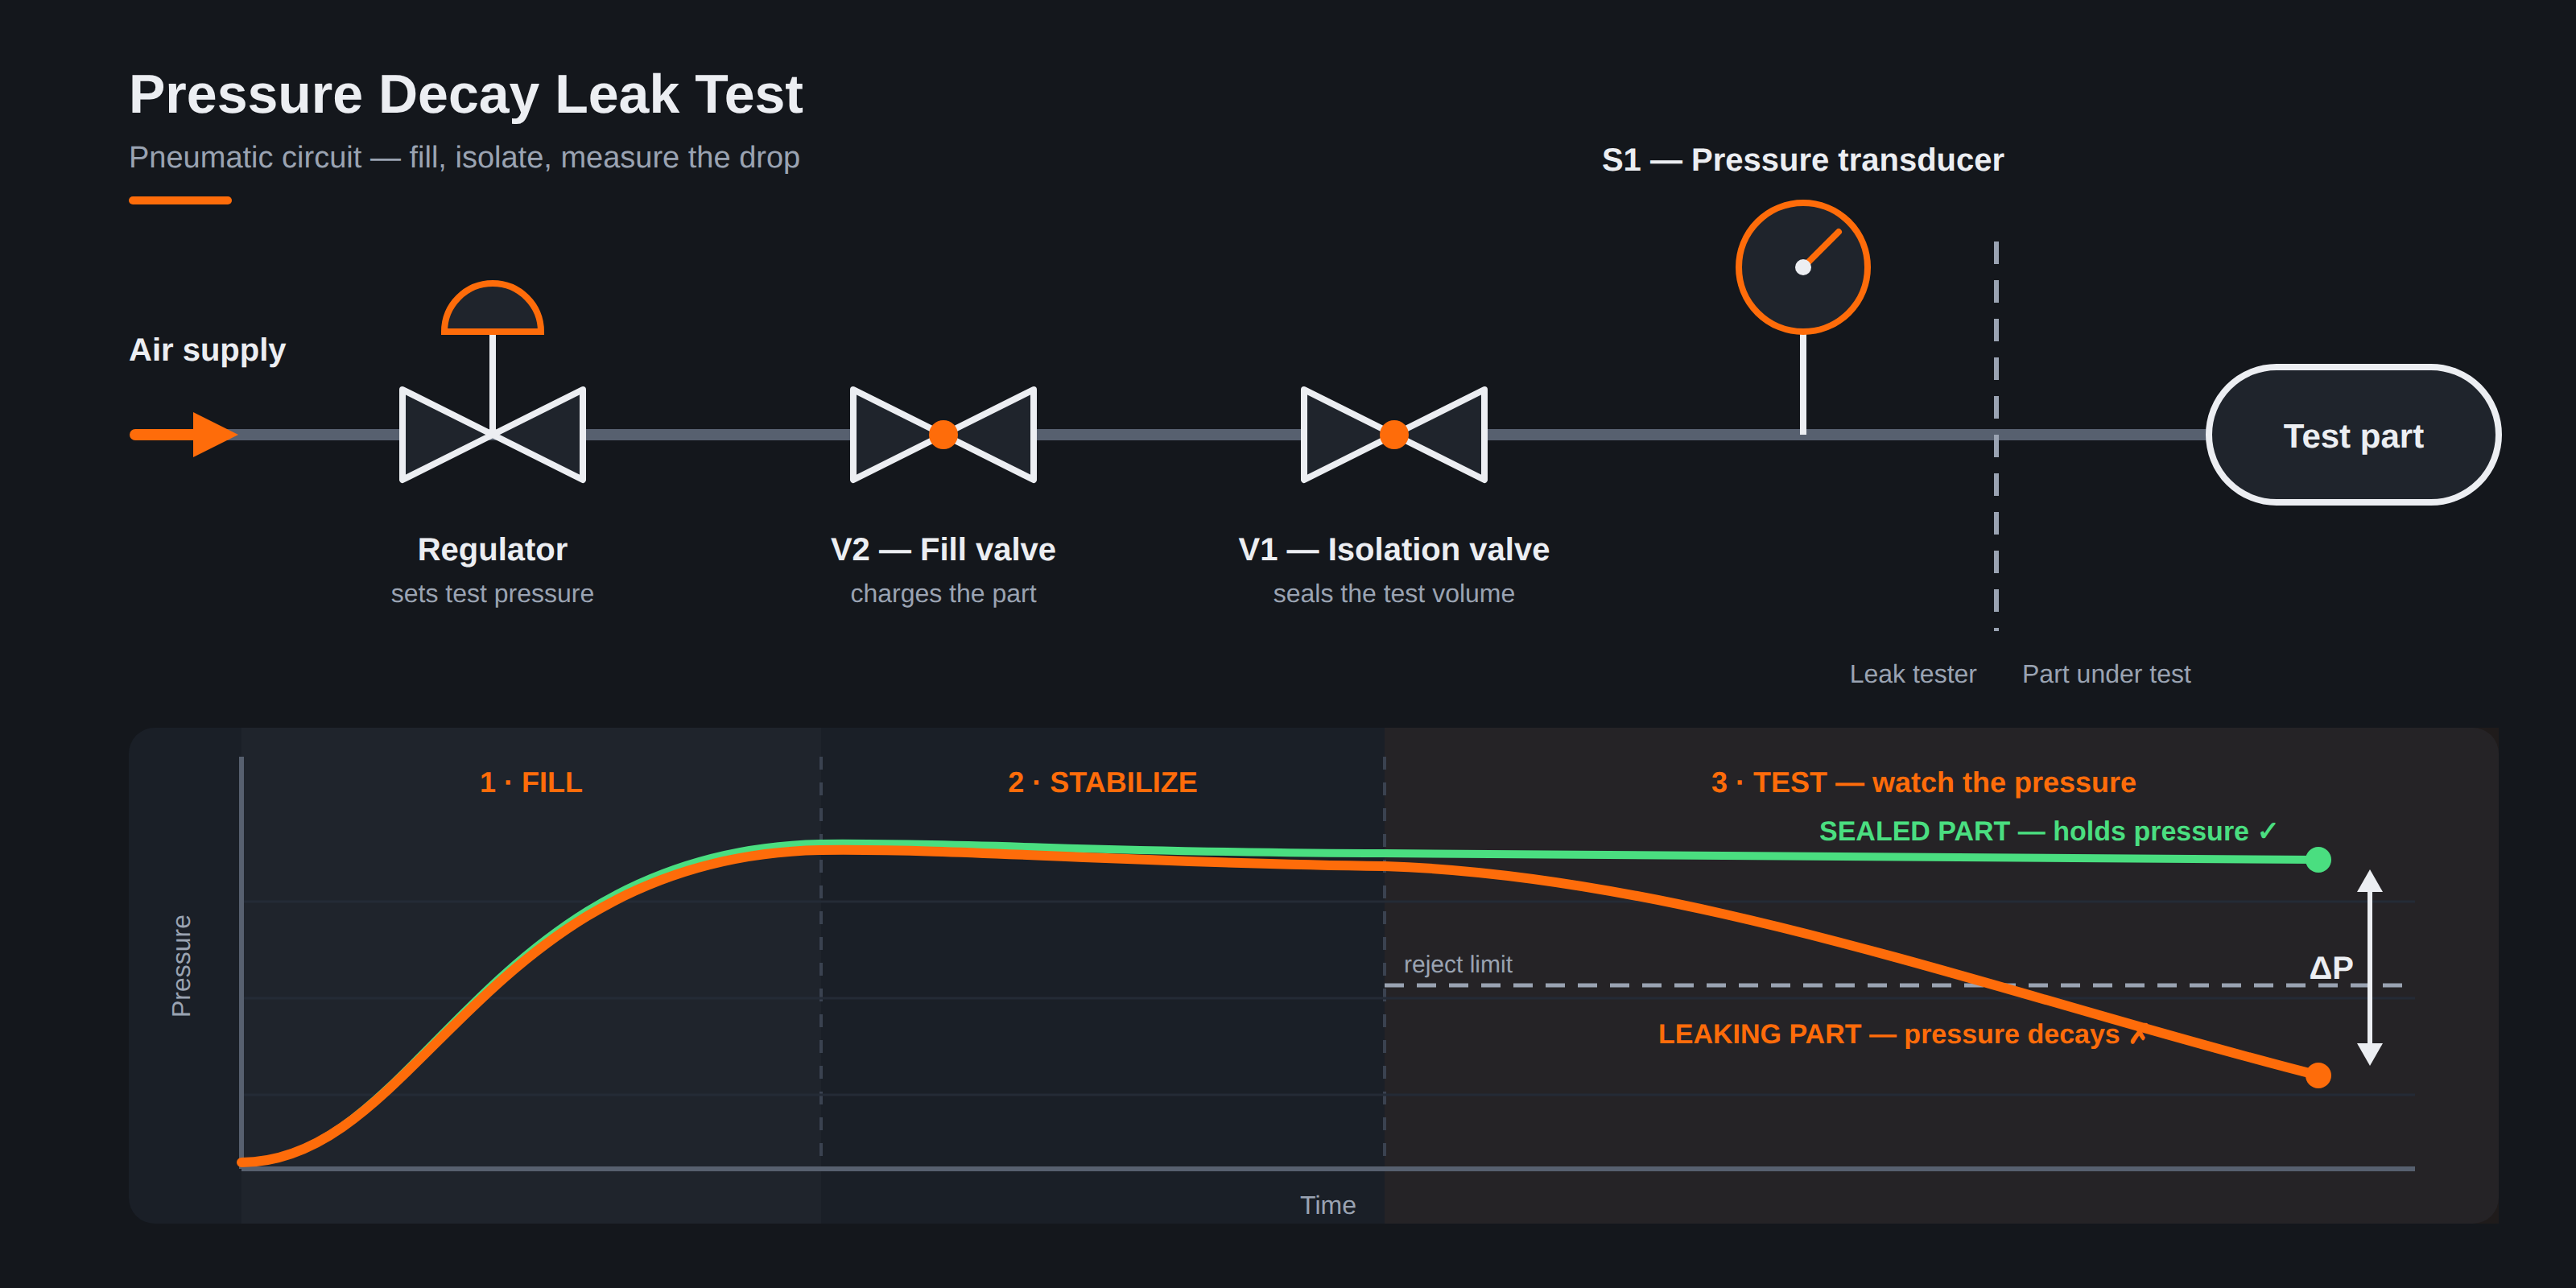
A pressure decay leak test pressurizes an internally pressurized part, isolates the air source, and measures any pressure drop over time to make a pass/fail decision.
Pressure decay is one of the most widely used leak-testing methods in manufacturing. It is suited to a sealed component with an access port and starts by connecting the part to a leak tester with a fitting or fixture.
After the part is pressurized, the air source is valved off and the pressure is allowed to settle. The test then measures the change in pressure over time against the programmed reject value.
Part volume and test time work together. Larger internal volumes need a longer cycle to reach a useful sensitivity, while smaller volumes can use shorter cycles and support higher production throughput.
Request for QuoteA pressure decay test answers one question: does this part hold pressure? The part is connected to the tester, filled to its test pressure, then sealed off from the air supply. From that moment the tester watches the pressure. Air escaping through a hole, a bad weld or an imperfect seal shows up as a falling pressure reading.
It is the most widely used leak test in manufacturing because it needs nothing more than air, a fitting and a repeatable sequence. There is no tracer gas to buy, no chamber to evacuate, and the part comes off the fixture unharmed, so every unit on the line can be tested rather than a sample.
The result is a pass or fail against a reject limit you set for that part. A pressure decay test tells you a part leaks more than you allow — it does not tell you where the leak is. When the location matters, a helium sniffer is the tool for that job.
Connect the part with a fitting or fixture and pressurize it to the desired test pressure.
Allow the part to settle after fill. This stage accommodates part stretching, flexing and thermodynamic stabilization before measurement.
The pressure sensor measures any drop in pressure during the test interval.
Vent the remaining system pressure to atmosphere; venting has no bearing on pass/fail and is for operator safety.
A non-leaking part remains within its specified pressure-decay limit and passes; a part that decays beyond its lower limit fails.
Zaxis testers resolve pressure to 0.00001 PSI. That resolution is what makes short cycles possible: the smaller the pressure change you can see reliably, the less time you need to spend watching for it.
Sensitivity is a negotiation between the part's internal volume and the time you give the test. The same leak bleeds a large volume slowly and a small volume quickly, so a big assembly needs a longer test interval to produce a measurable drop, while a small sealed component can be judged in a fraction of the time. That is why small-volume parts run at high throughput on the same tester that needs a patient cycle for a large one.
Settle time exists because parts move. A flexible part stretches when it is pressurised, and that expansion looks exactly like a leak to a pressure sensor. Settle gives the part time to stop moving so the test interval measures leakage instead of elasticity.
Temperature and fixturing deserve the same attention. Compressed air warms as it fills and cools as it settles, and a fixture that flexes adds volume of its own. A stable fixture, a consistent fill and a settled part are what turn 0.00001 PSI of resolution into a trustworthy production decision.
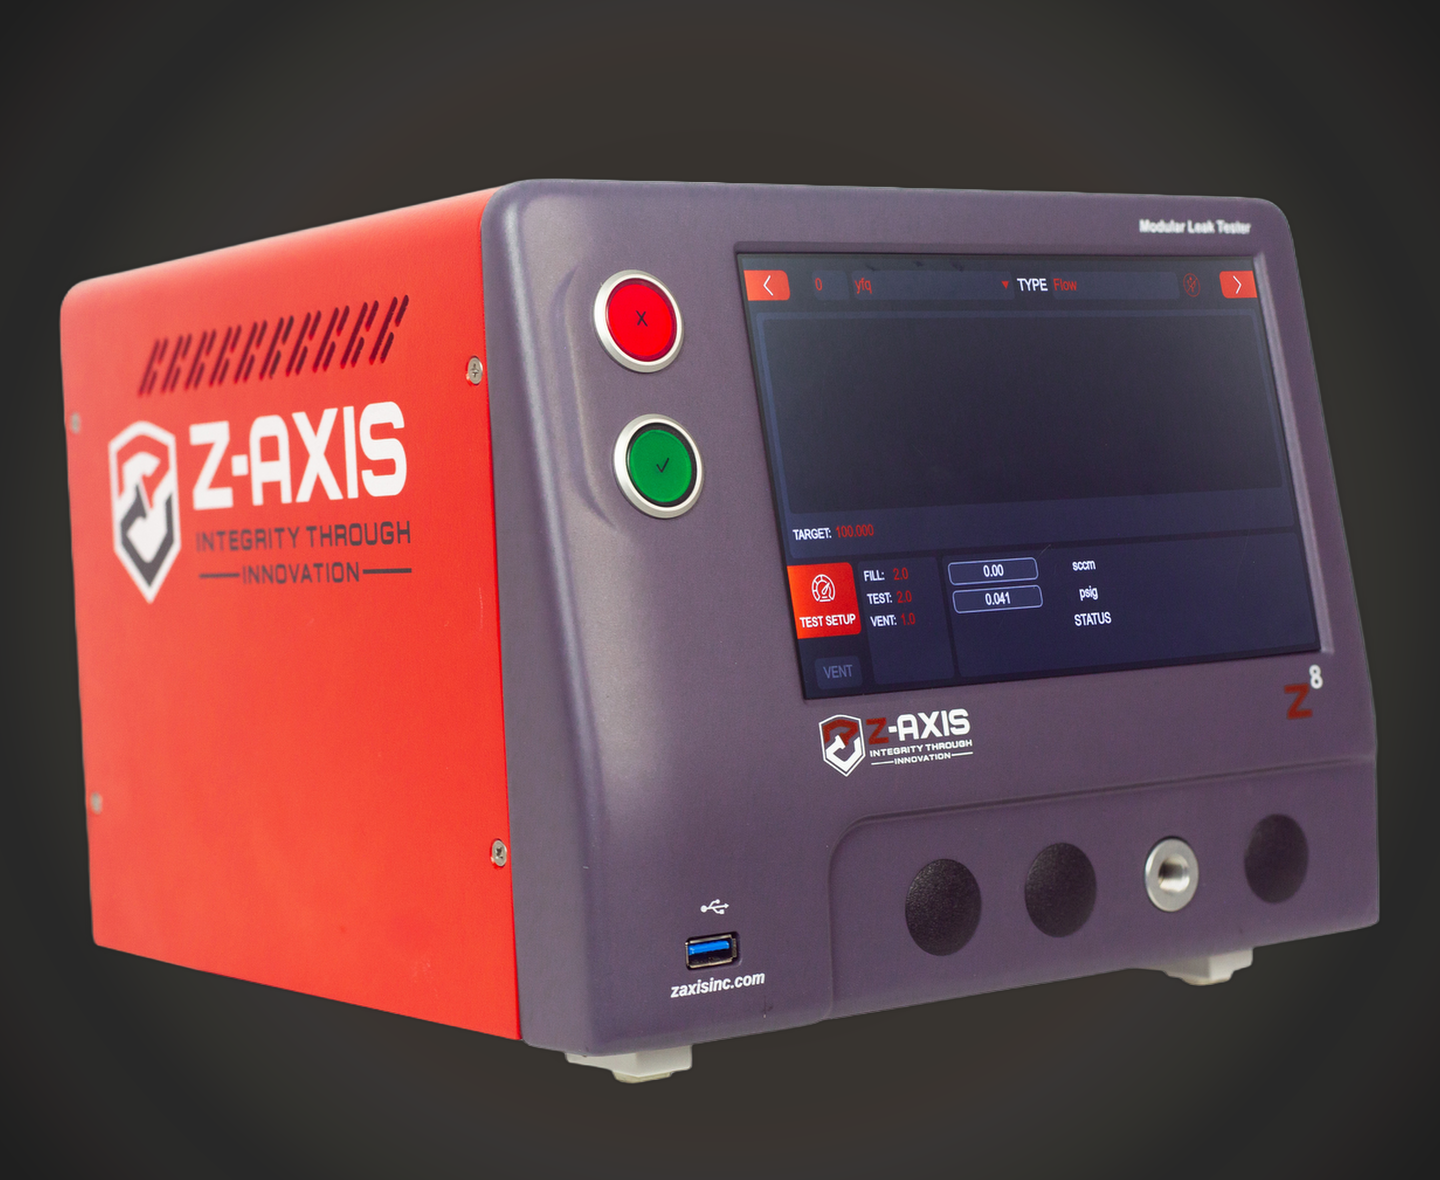
Every Zaxis air leak tester runs pressure decay. They differ in channel count, interface and enclosure, so the choice comes down to where the tester has to live and how many parts it has to handle.
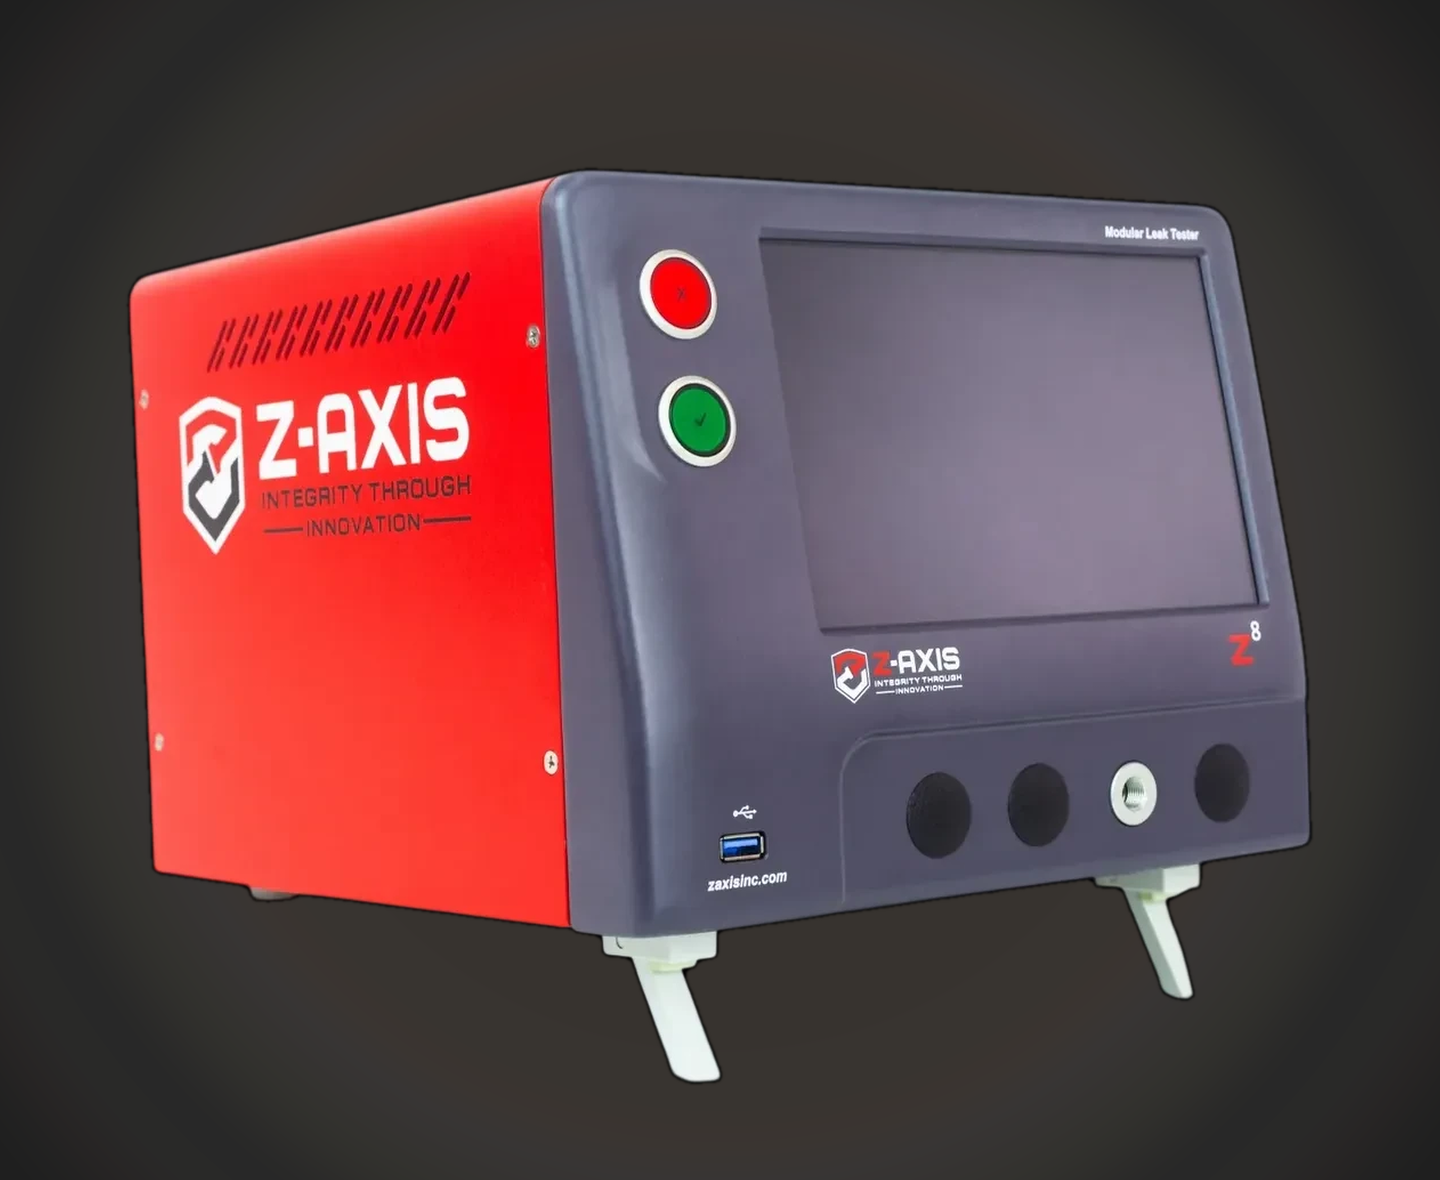 Z8Up to four channels, an 8-inch touchscreen, and pressures to 1000 PSIG for automated production lines.
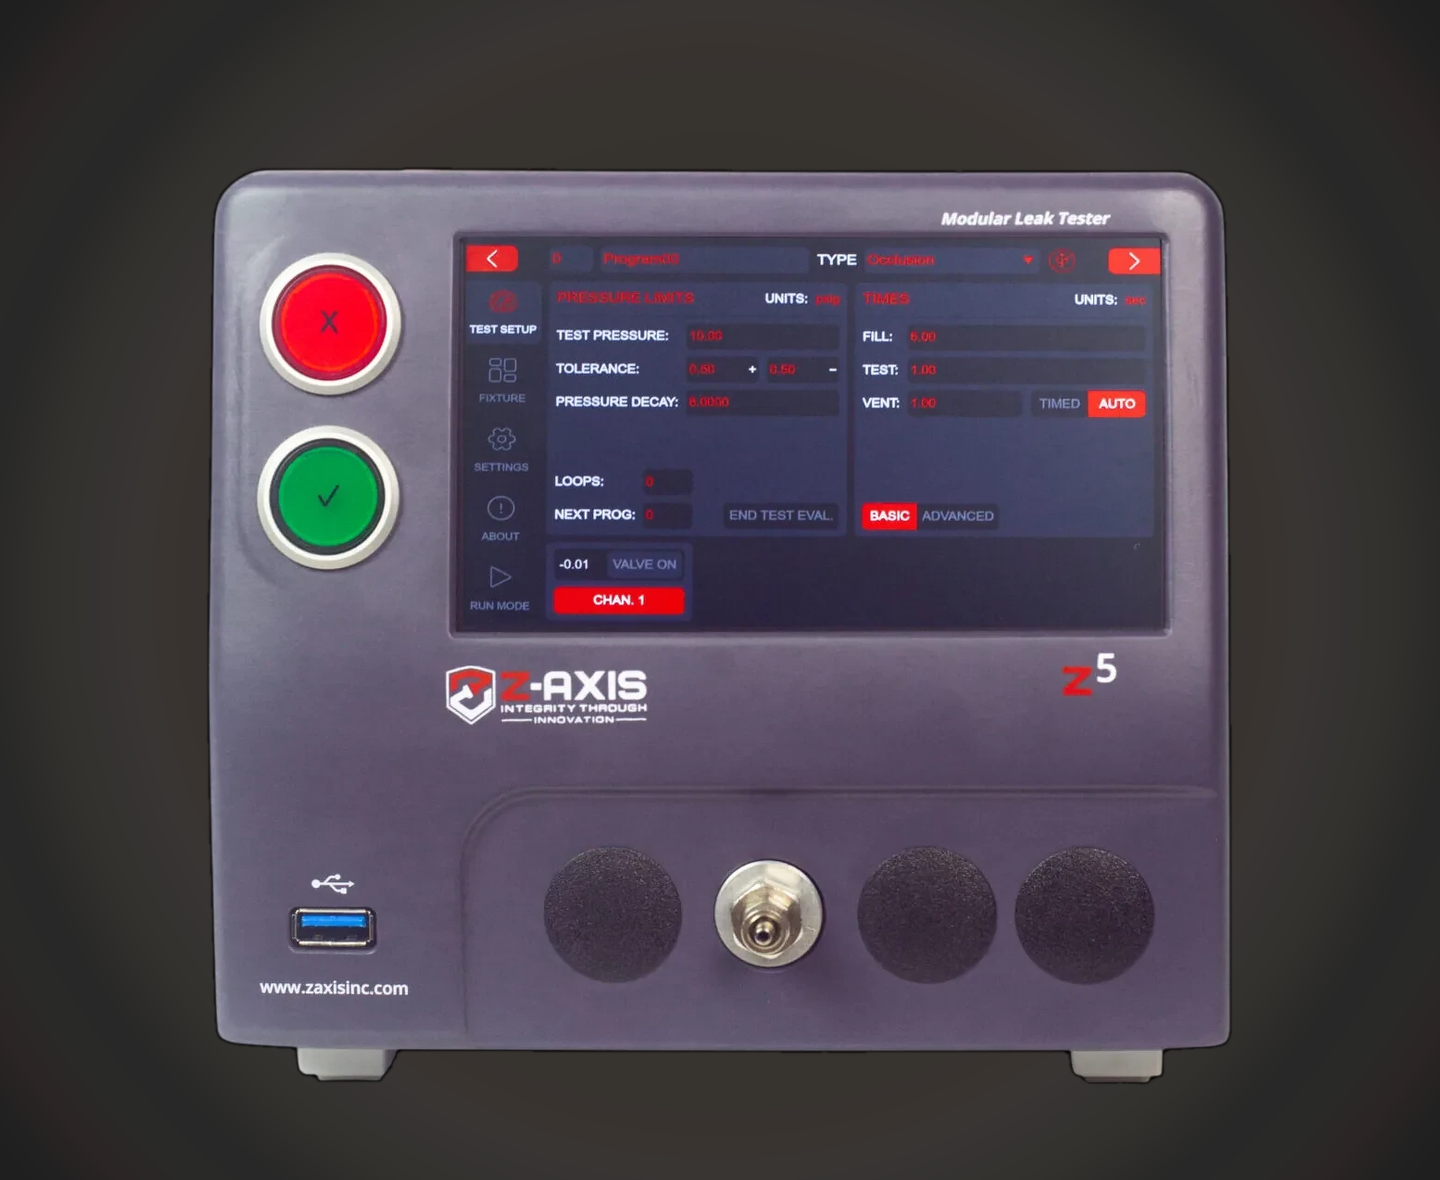 Z5The benchtop workhorse: 5-inch touchscreen, the same 0.00001 PSI resolution, in a 6.5-inch-wide cabinet.
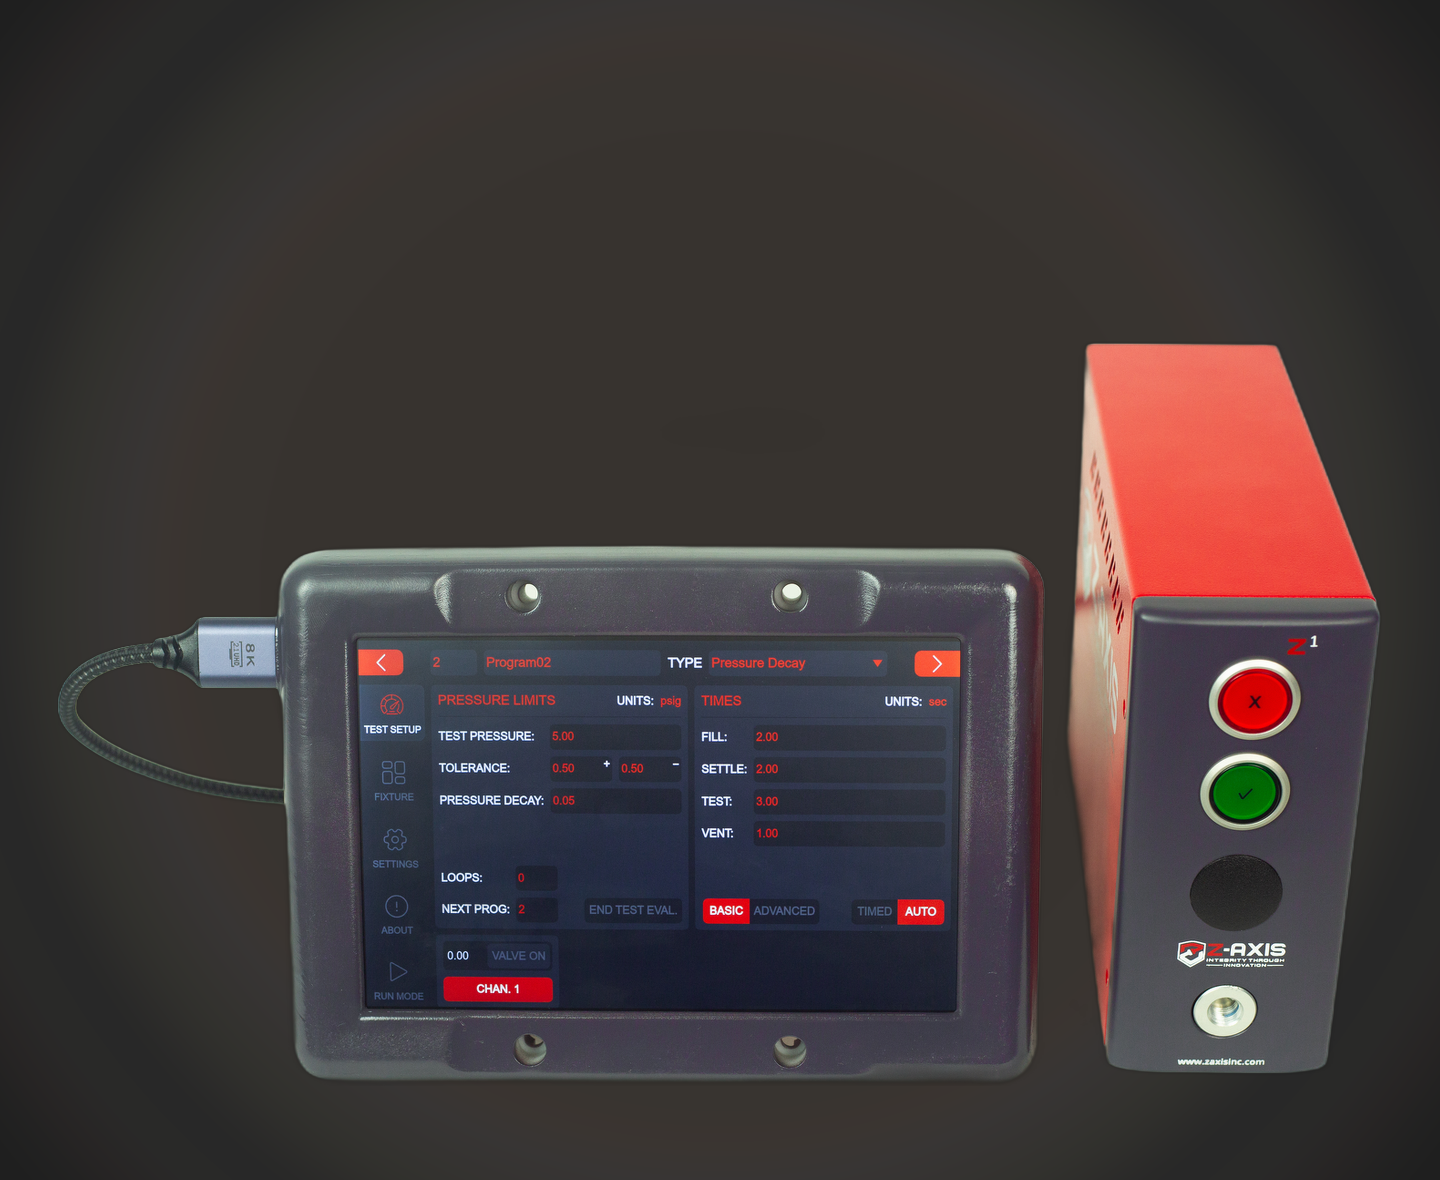 Z12.6 inches wide with an optional detachable touchscreen, built to live inside a machine.
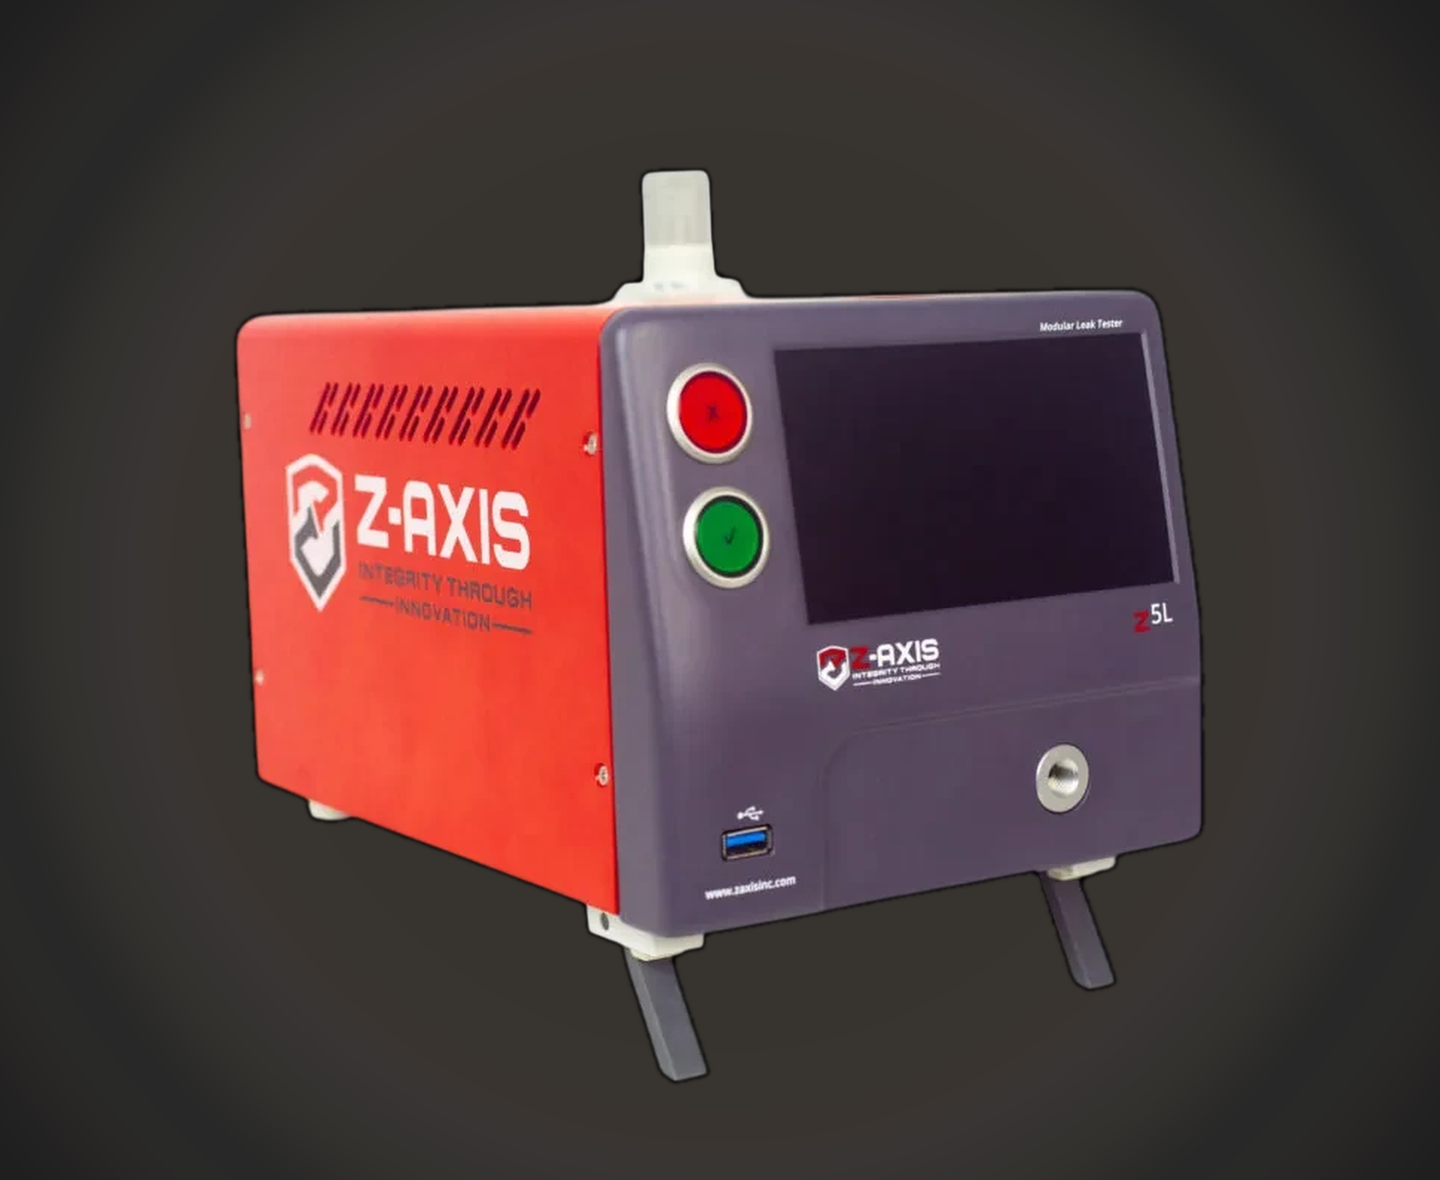 Z5LSingle-channel entry point, 0–30 or 0–100 PSIG, with single-screen test setup.
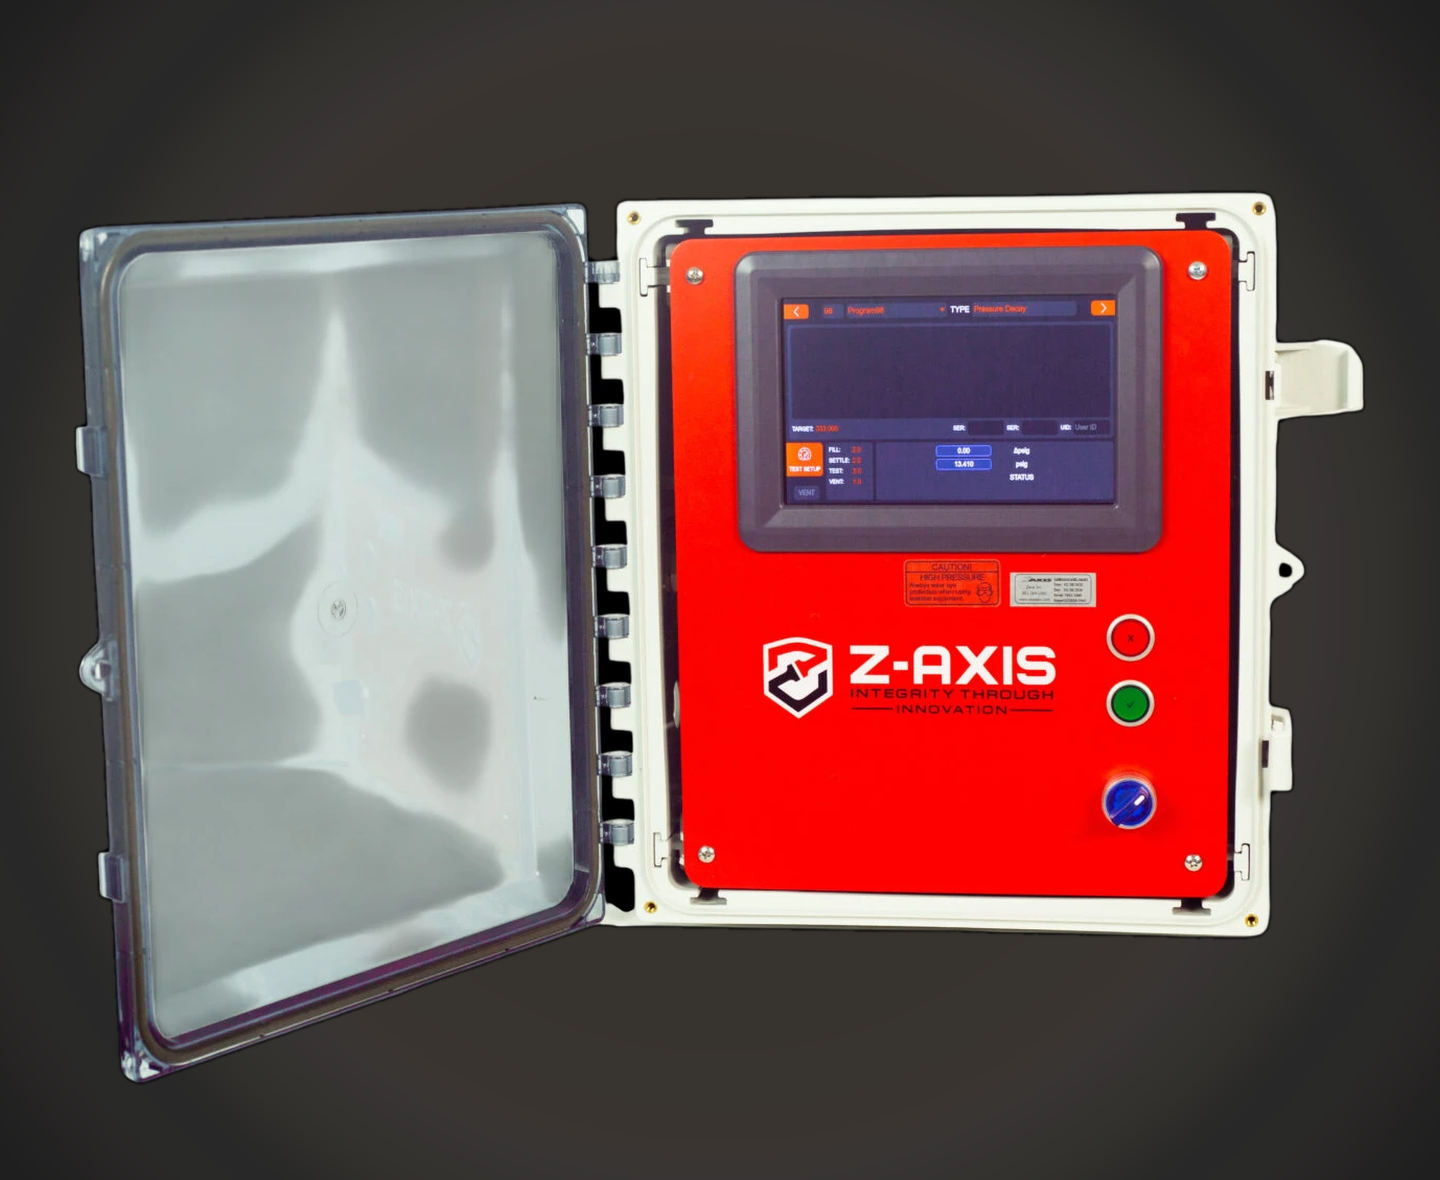 Z8NZ8 capability inside a sealed NEMA enclosure for dusty or washdown areas of the plant.
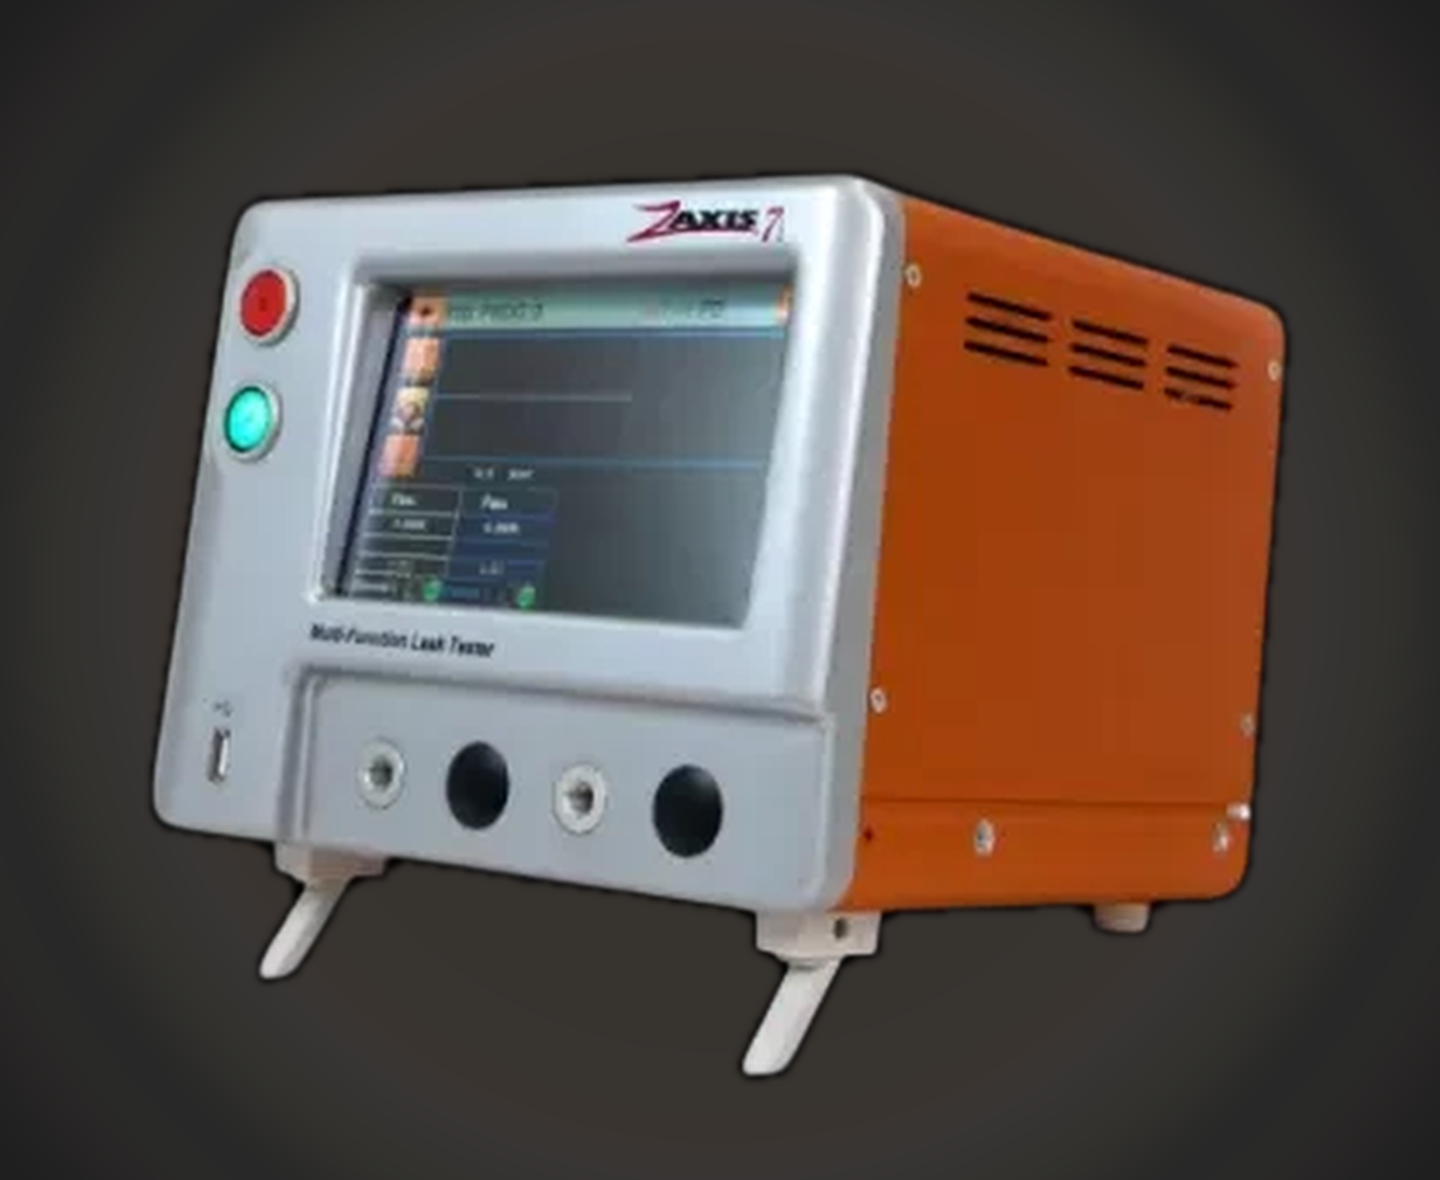 VM3Generates its own fixed air volume with a plunger, so a station needs no house air supply.
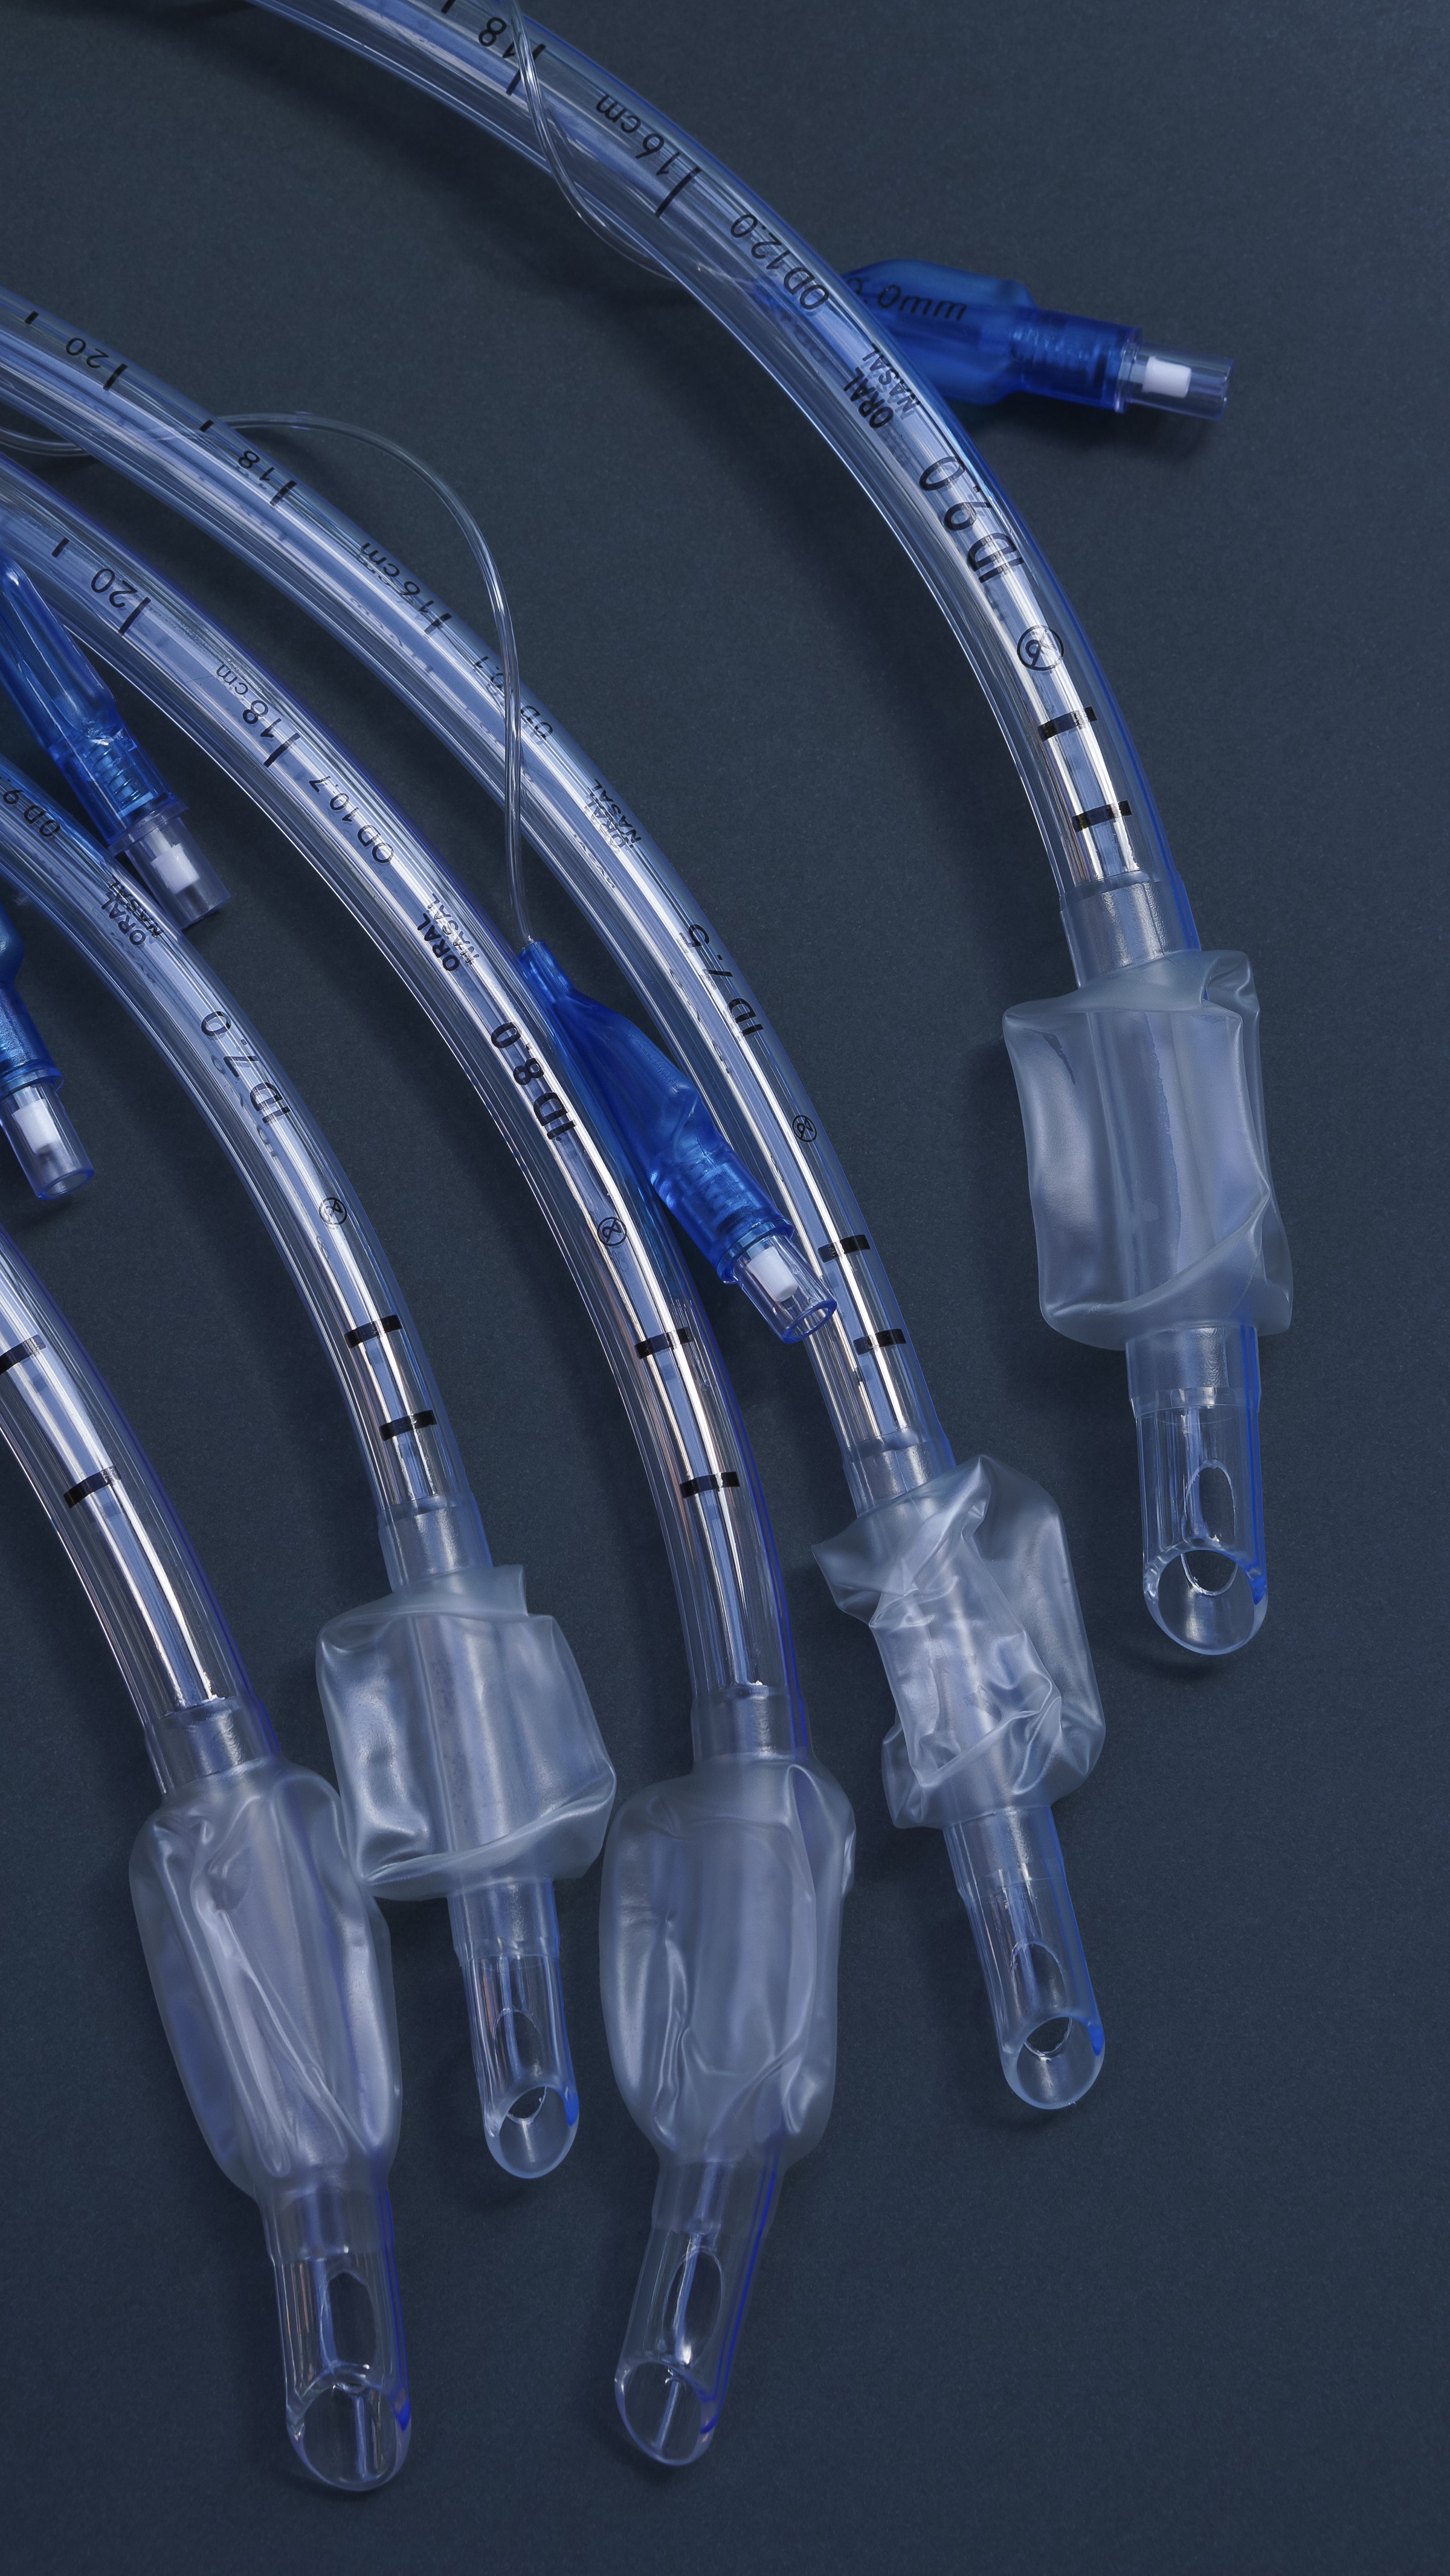
Balloon catheters, IV sets, infusion sets and needleless injection components are pressure decay's home ground: sealed, low volume, and required to hold pressure in use.
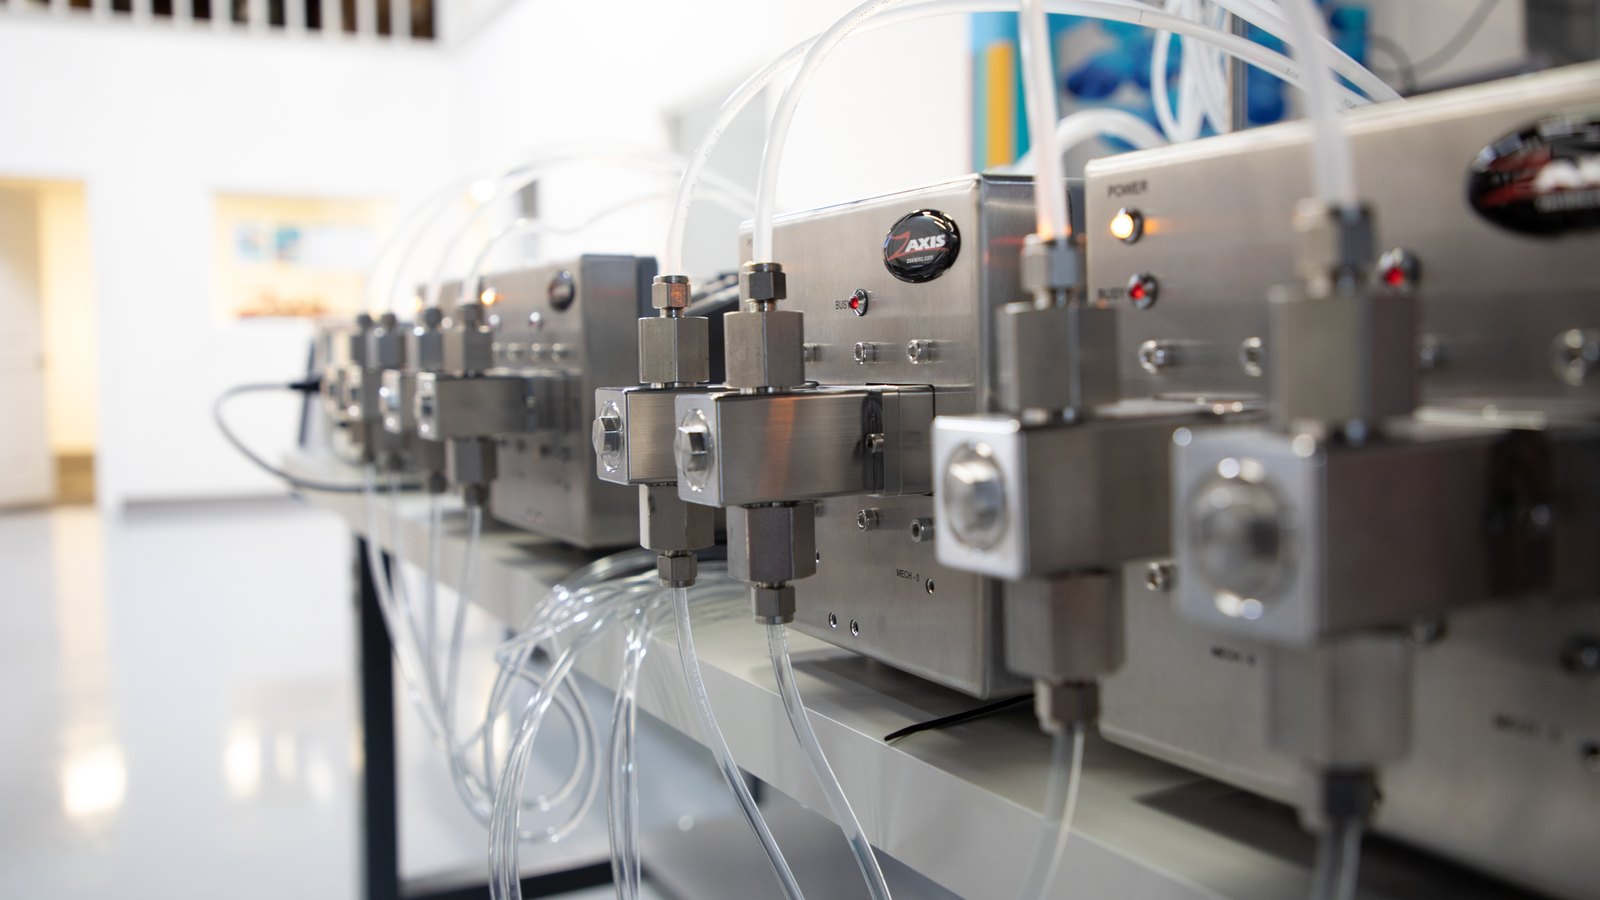
Devices that carry fluid inside the body are tested unit by unit, which suits a non-destructive method that leaves the part fit to ship.
Enclosures that must keep moisture out are checked through a single port, with the tester generating its own air volume when no plant air is available.
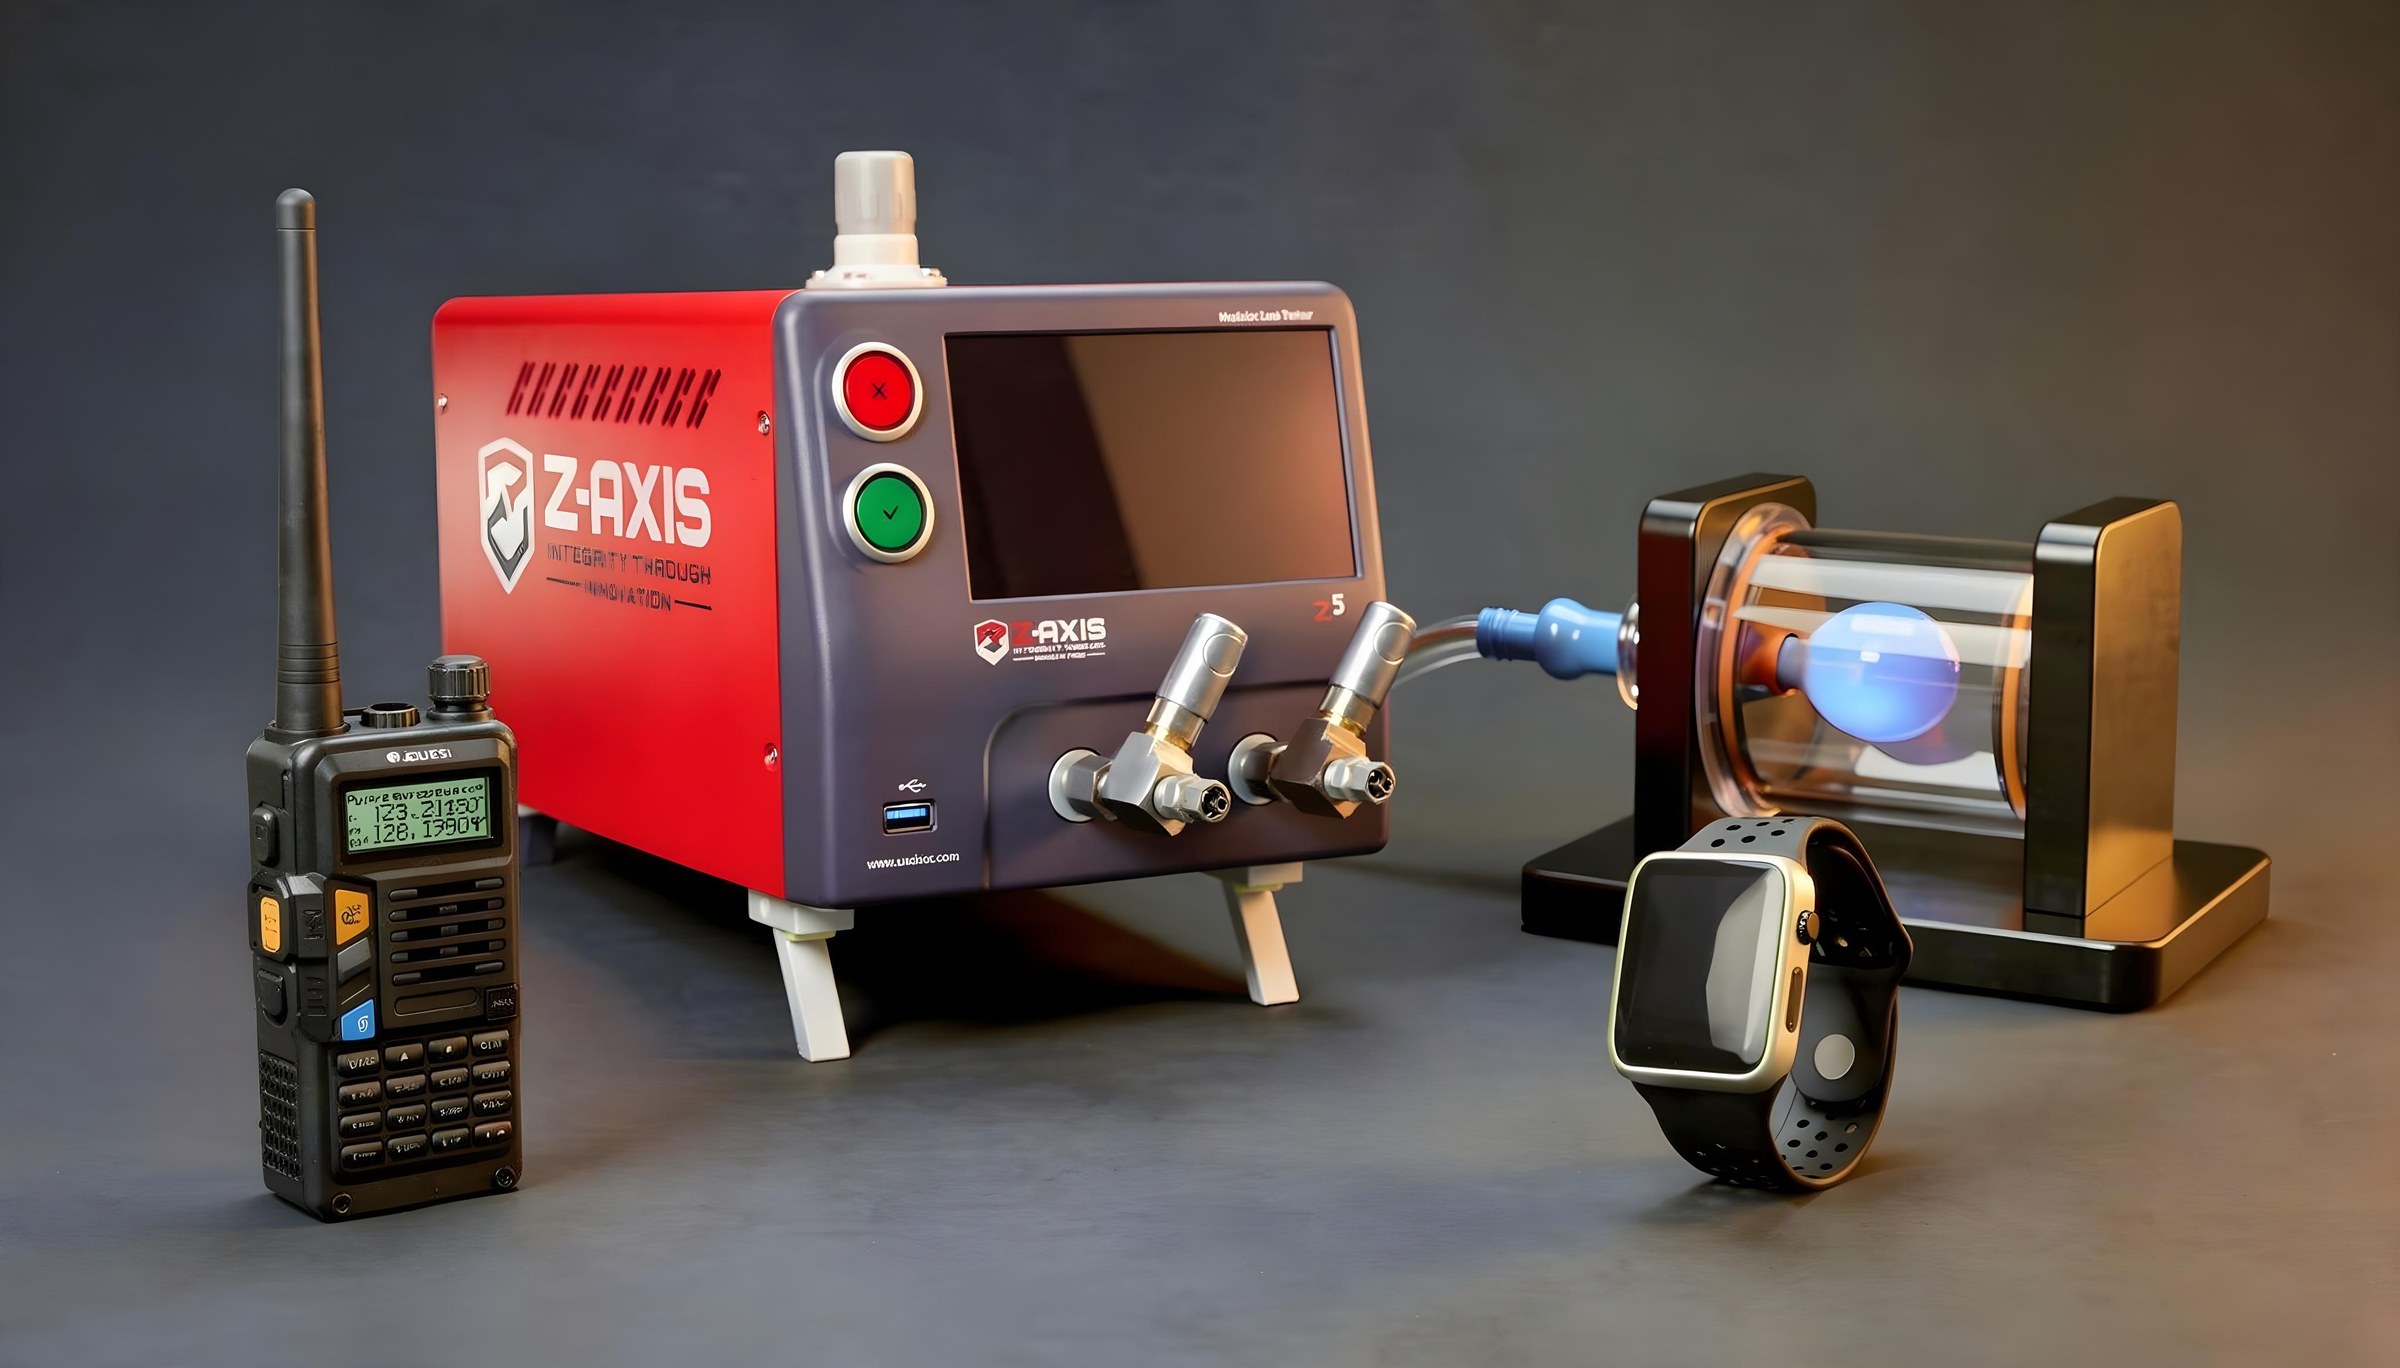
Bags, pouches and sensor housings without a usable port are tested inside a chamber fixture, where the same decay measurement is made on the space around the part.
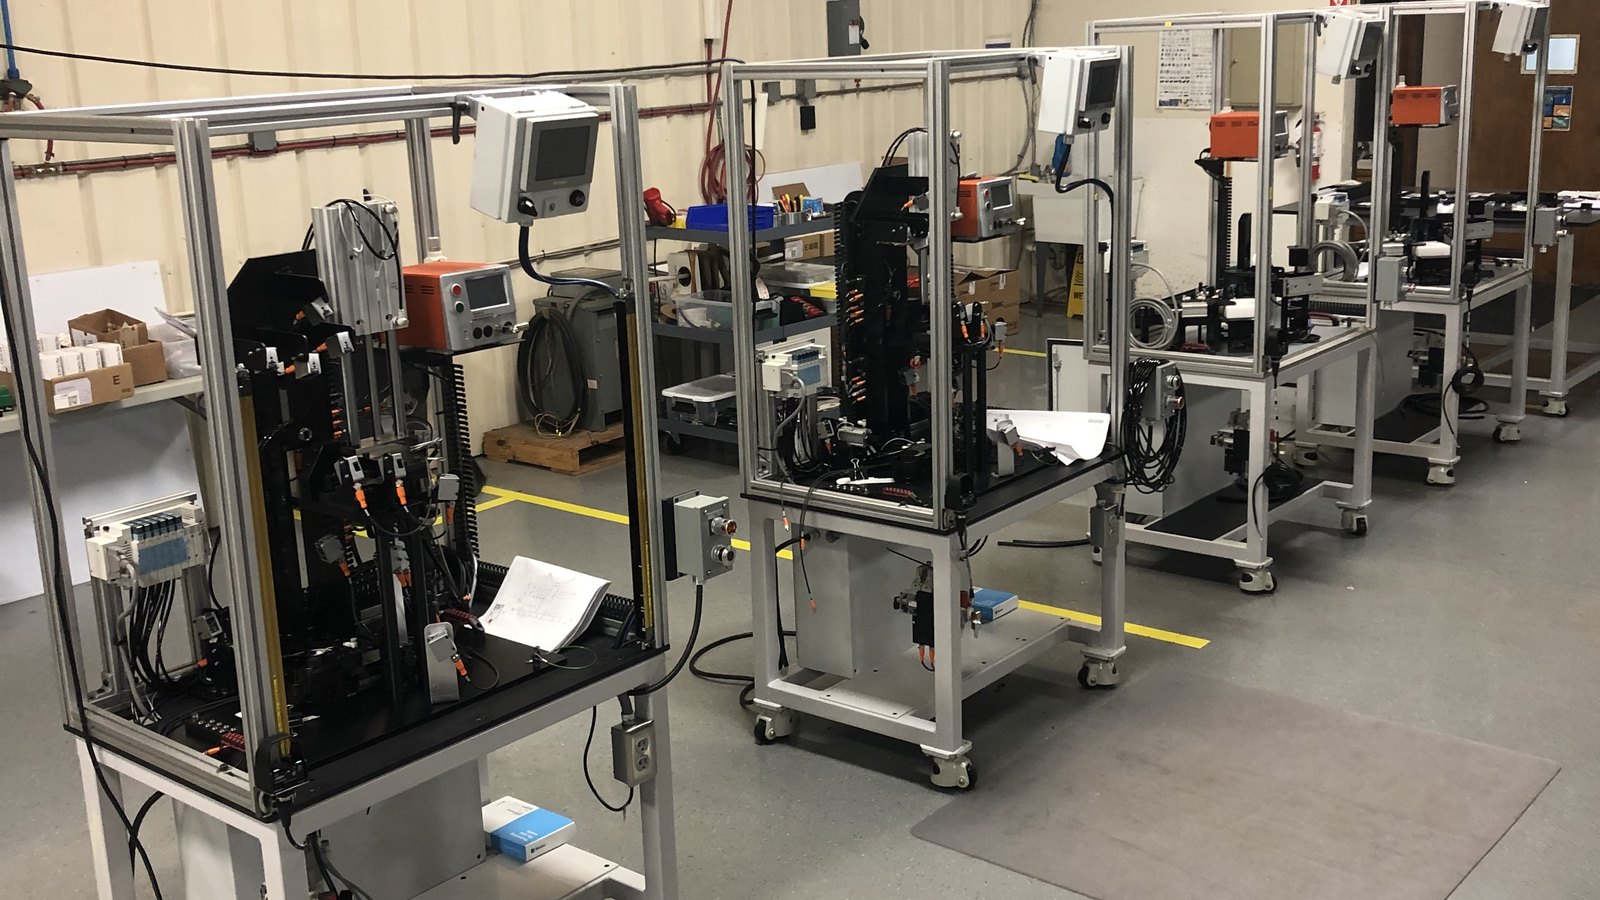
A single-channel tester mounts beside its fixture and runs one recipe on cue from the machine, which is how pressure decay ends up embedded in an assembly line rather than beside it.
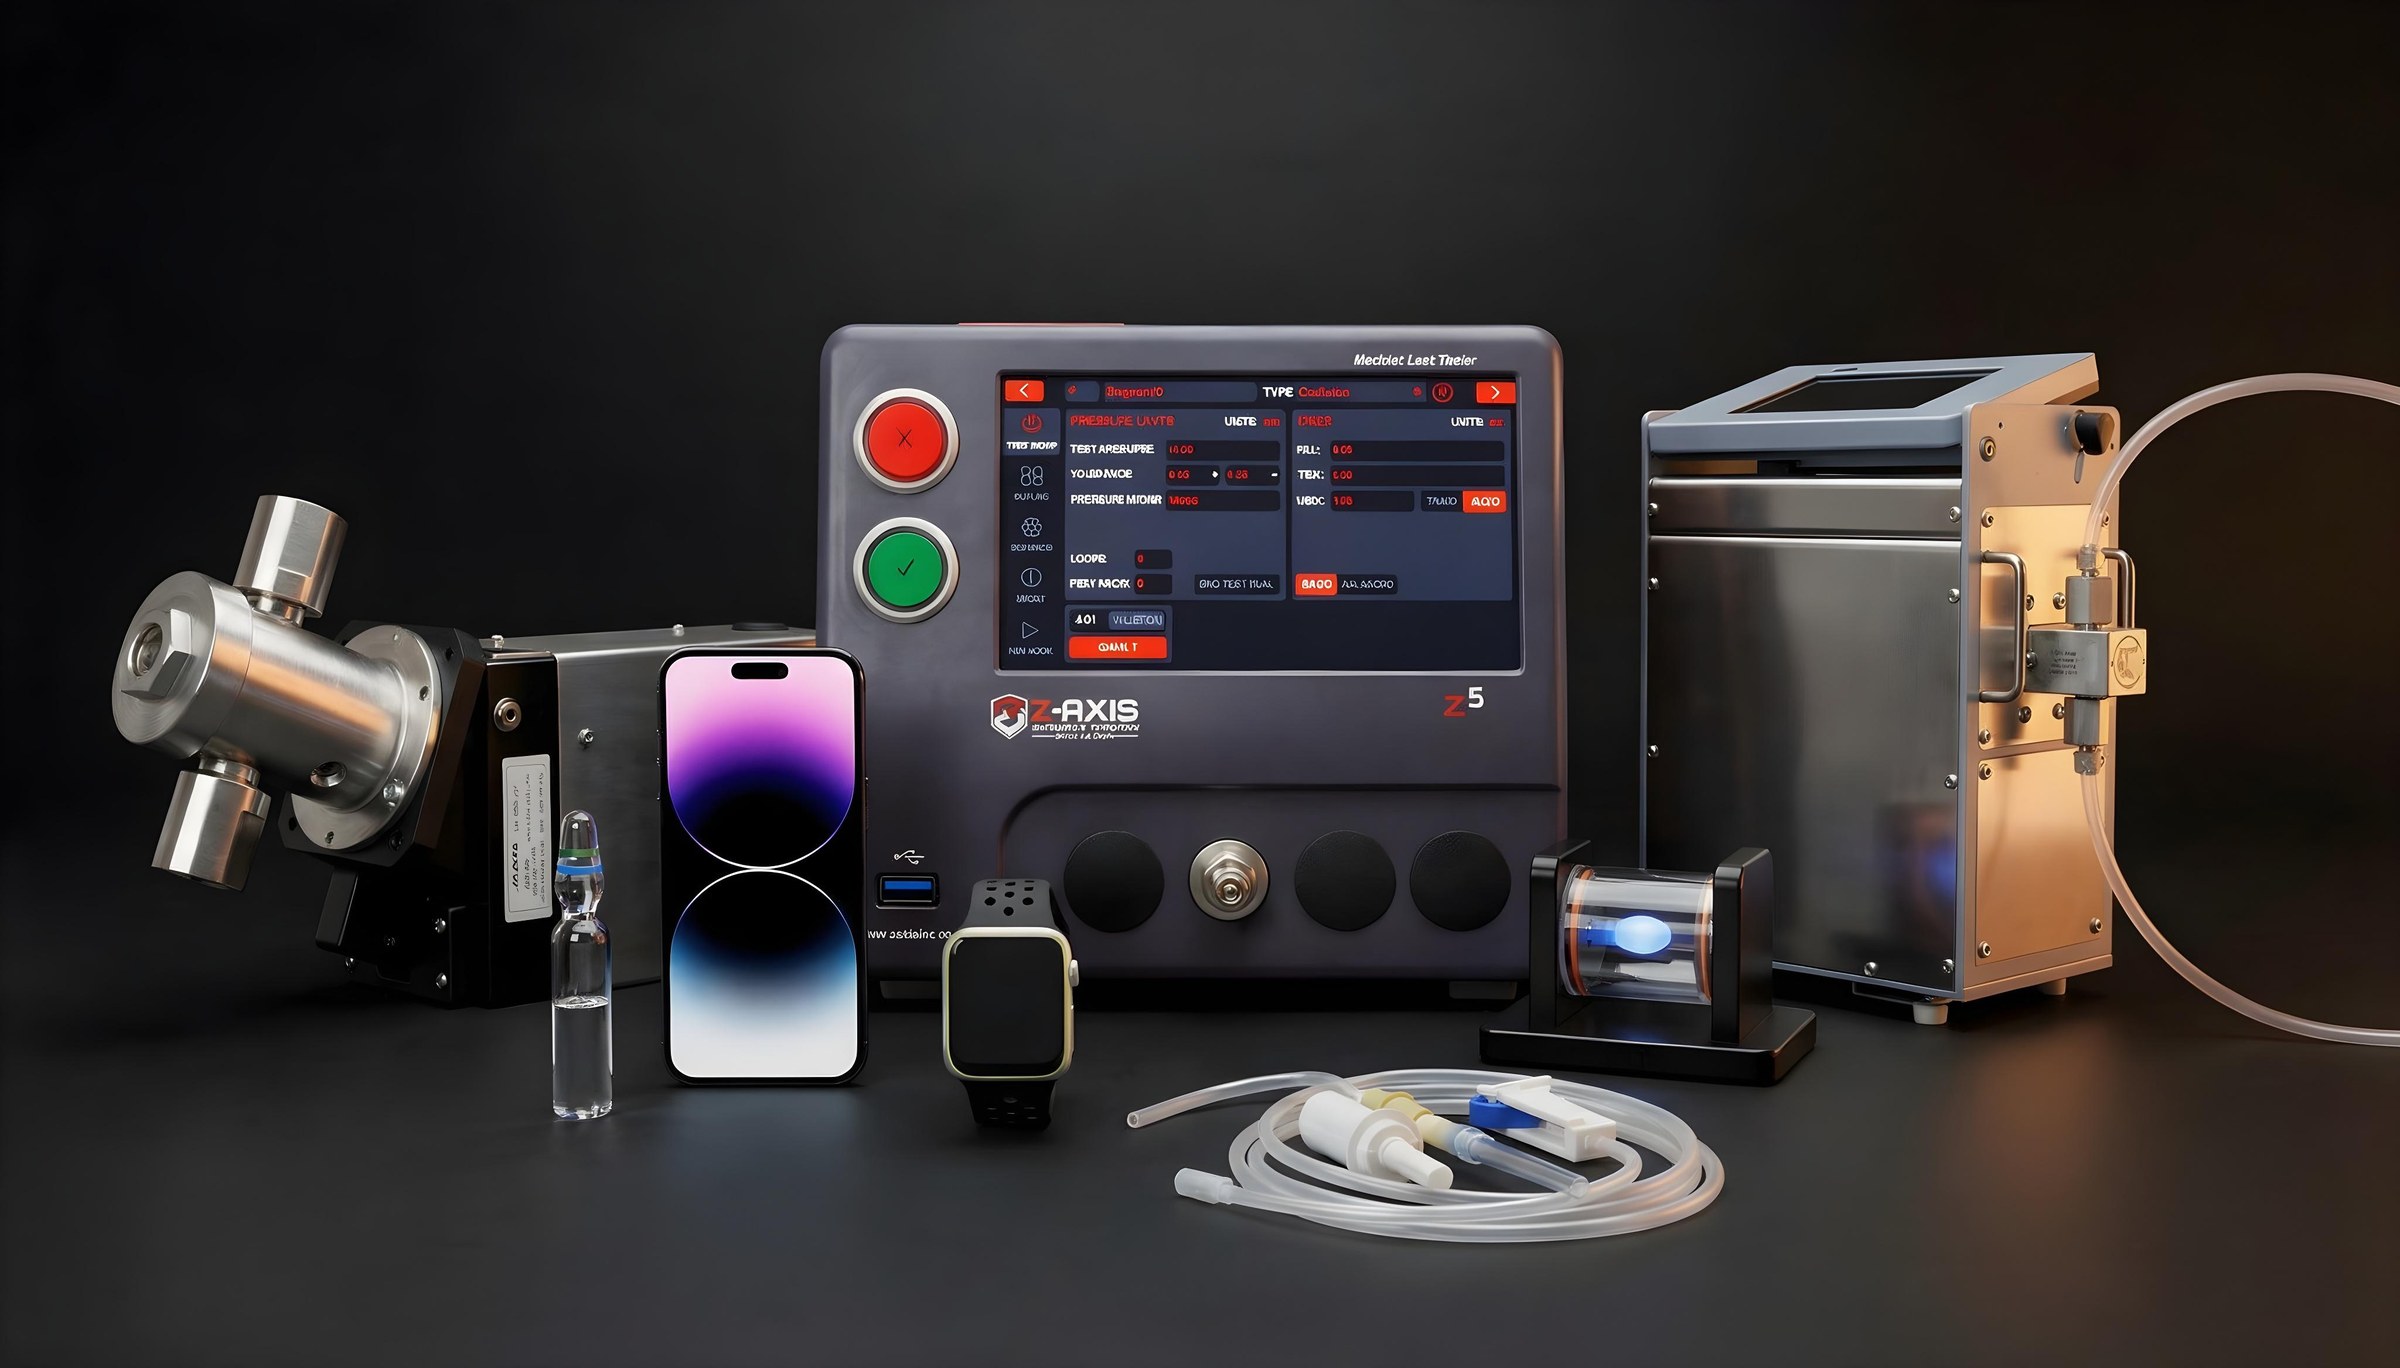
Parts with several sealed cavities are tested on separate channels so a failure points at a specific cavity instead of the whole assembly.
| Method | Non-destructive | Needs an access port | Locates the leak | Typical use |
|---|---|---|---|---|
| Pressure decay | ✓ | ✓ | × | Sealed parts with a port |
| Vacuum decay | ✓ | ✓ | × | Parts and packaging |
| Mass flow | ✓ | ✓ | × | Flow-rate limits |
| Occlusion | ✓ | ✓ | × | Blocked passages |
| Burst | × | ✓ | × | Failure pressure |
| Pressure cracking | ✓ | ✓ | × | Valve opening pressure |
| Chamber | ✓ | × | × | Sealed parts, no port |
| Sniffing | ✓ | ✓ | ✓ | Finding the leak site |
| Hard vacuum | ✓ | ✓ | × | Hermetic, safety-critical parts |
| Accumulation | ✓ | ✓ | × | Large parts, total leak rate |
| Bombing | ✓ | × | × | Sealed parts, no fill port |
| Differential pressure | ✓ | ✓ | × | Large volumes, low leak rates |
| Trace gas | ✓ | ✓ | ✓ | Very small leaks, quantified |
It pressurizes a sealed part, isolates the air source, and measures the pressure change over time. A drop in pressure during the test signifies a leak.
Zaxis testers resolve pressure changes to 0.00001 PSI. What that converts to as a leak rate depends on your part's internal volume and how long the test interval runs.
Cycle time depends on part volume and the time needed to reach the required sensitivity. Typical production cycles are often 7–10 seconds; larger volumes need longer cycles and appropriately sized valves to fill and vent efficiently.
Yes. Large internal volumes require more cycle time to reach useful sensitivity; smaller internal volumes can support faster cycles.
Settle time follows fill and allows the part to accommodate stretching or flexing before pressure decay is measured.
Pressure decay applies positive pressure and measures a pressure drop. Vacuum decay applies negative pressure and measures an increase in vacuum pressure.
No. It makes a pass/fail decision from pressure change. Sniffing leak testing is used when the physical leak location is needed.
No. It is a non-destructive method for sealed components.
Test pressure is chosen for the part and its application, not by the method. Across the Zaxis range the available spans run from 2 PSIG up to 1000 PSIG of positive pressure, plus vacuum to roughly -14.7 PSI, and the tester is configured for the span your part needs.
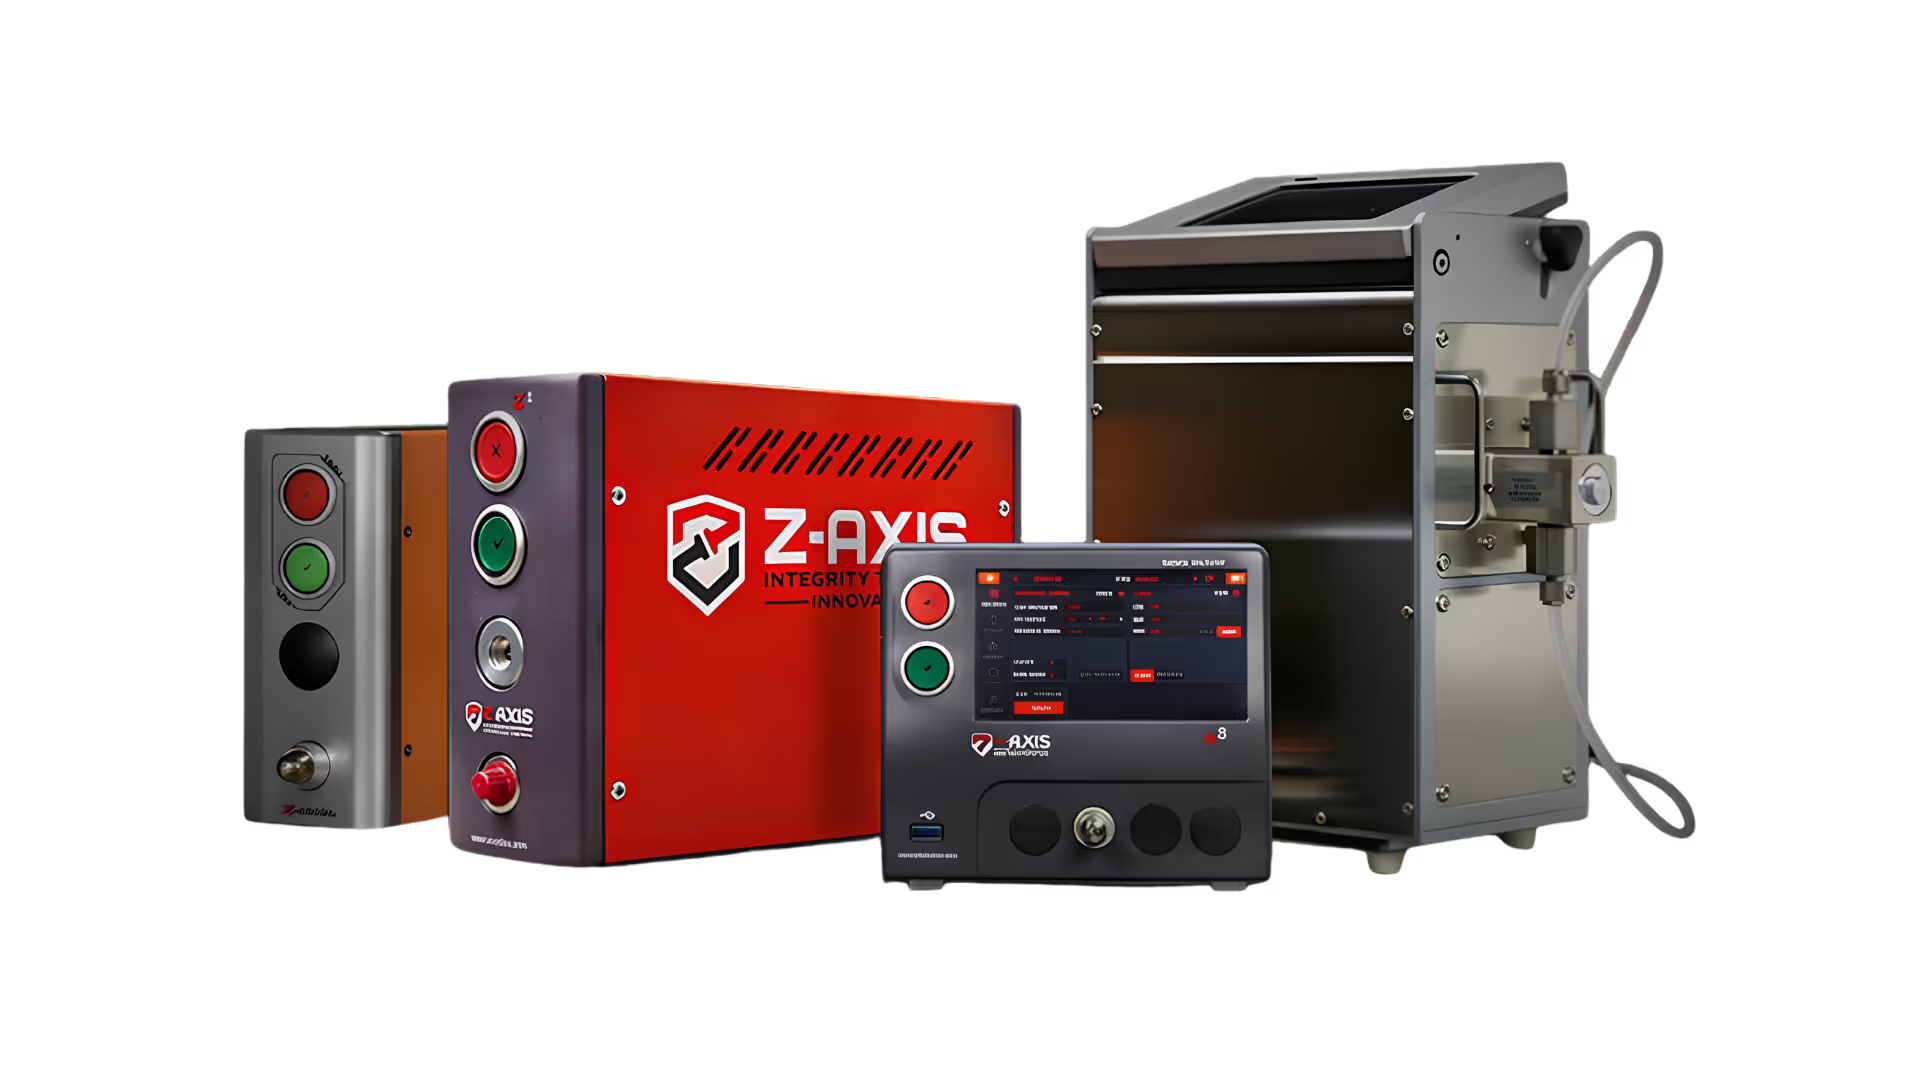
Planning a production station? Read the Pressure Decay Leak Testing Buyer’s Guide and compare alternatives in the leak test method chooser.
For standards scope context, see the ASTM F2095 and ASTM E2930 explainers.
For HVAC and refrigeration components, see HVAC & Refrigeration Leak Testing; for package CCI context, see Pharmaceutical & Medical Packaging Leak Testing.
Planning a production station? Read the Pressure Decay Leak Testing Buyer’s Guide and compare alternatives in the leak test method chooser.
Plan the test boundary with the Leak Test Fixture Design Guide and review IP67 / IP68 production leak testing for ingress-driven enclosure programs.